

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com


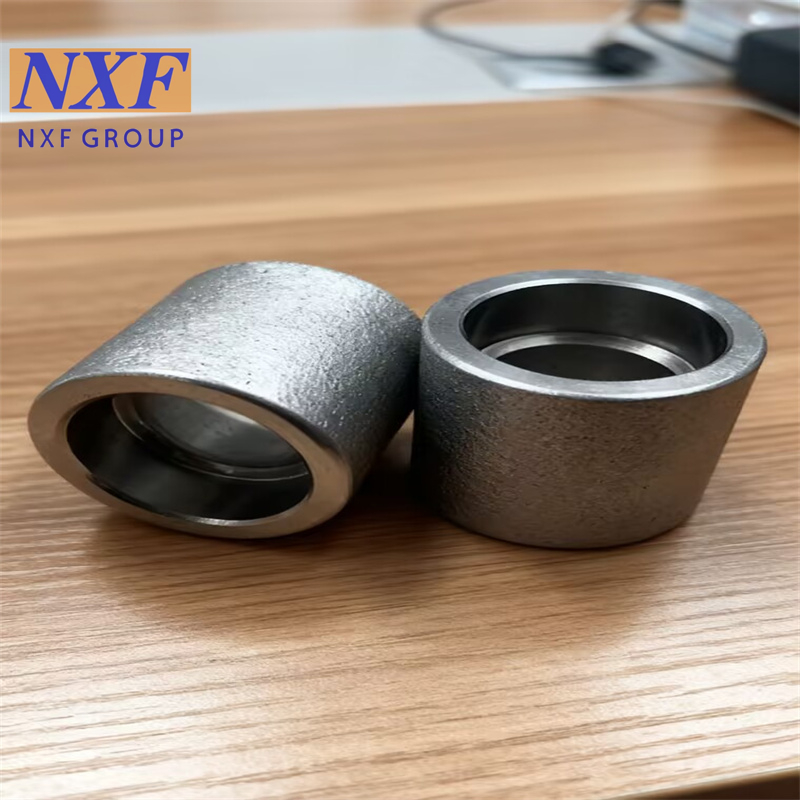
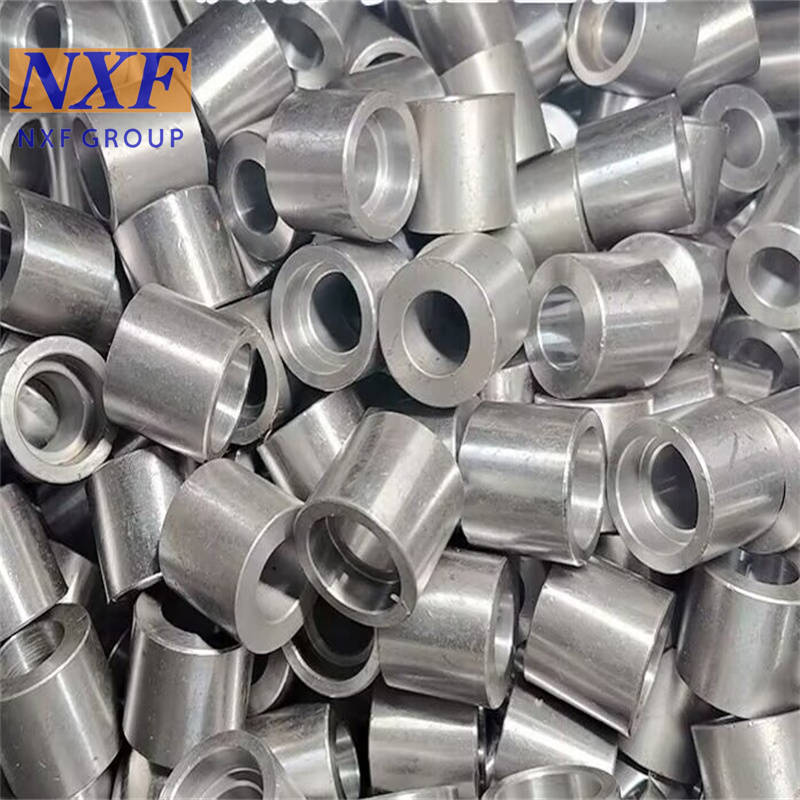
NXF UNS N04400/Monel400/NiCu30Fe/Alloy 400/NCu30 DN15-1200 Class3000-9000 High Pressure Fitting Socket Welding Coupling
Key Features & Function
* Connection Method: Pipe is inserted into a socket (like a female end), then a fillet weld is applied to the exterior joint.
* Application: Primarily for smaller pipes (often under 4 inches) in demanding, high-pressure, high-temperature environments.
* Types: Includes full couplings (connecting two pipes), half couplings (branching off a larger pipe), and reducing couplings
* Connection Method: Pipe is inserted into a socket (like a female end), then a fillet weld is applied to the exterior joint.
* Application: Primarily for smaller pipes (often under 4 inches) in demanding, high-pressure, high-temperature environments.
* Types: Includes full couplings (connecting two pipes), half couplings (branching off a larger pipe), and reducing couplings
(connecting different pipe sizes).
* Benefits: Offers strong, leak-tight connections, good flow, and simpler installation than butt-welding for smaller sizes, often using TIG for quality root passes.






1. who are we?
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material) We have our own factories, quality can be controlled seriously.We Specialize in manufacturing about 21 years.We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian
total 0 Sheet,Only 5 images can be uploaded, each less than 5m.