

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
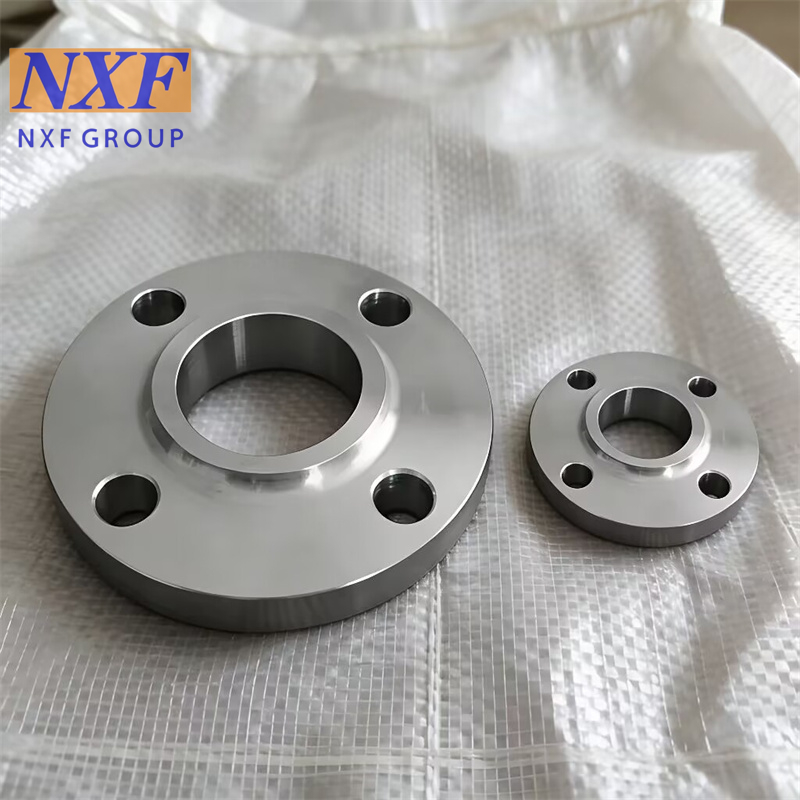
NXF UNS S32760 F55/S32760/1.4501 DN15-1200 Class150-1500 Super Duplex F55 Stainless Steel S32760 Slip on Flanges
crevice corrosion in seawater and other chloride containing environments, with critical pitting temperature that is more than 50°C(122°F). This material is known to also have high strength and extended lifecycle. It is 10% lighter than grade 316 steel,ideal for sub-zero service, and more cost effective than nickel alloys. Stainless steel grade F55 can be easily machined and welded. The following datasheet provides an overview of stainless steel grade F55.




1. who are we?
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material) We have our own factories, quality can be controlled seriously.We Specialize in manufacturing about 21 years.We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian