

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
NXF UNS S20910 XM-19 OD DN6-DN1200 Pressure 3000-9000lb Special Stainless Steel Forging Threaded 45 Degree Elbow
UNS S20910 XM-19 Stainless Steel Introduction
magneticpermeability of this alloy allows it to be used as a material for medical implants.
Machinability
Stainless steel grade UNS S20910 XM-19 has machinability characteristics that are similar to other austenitic stainless
steels;however it requires slower speeds, more power, and higher rigidity due to its high work hardening rate. It is recommended that coated carbide tooling be used.
Forming
Stainless steel grade UNS S20910 XM-19 can be formed using the same methods applied for other austenitic stainless steels. More power for forming and forging is needed for this alloy. Forging can be done at 1177-1204°C (2150-2200°F).
Welding
Welding of stainless steel grade UNS S20910 XM-19 can be performed using traditional joining processes. Recommended filler metal should be UNS S20910 XM-19 (AWS E/ER209).
Caution should be taken while using autogenous, high power density joining processes such as EB or laser welding, due to low FN potential and severe outgassing possibility.
Heat Treatment
Final annealing process performed for several of the applications, is done at 1065°C (1950°F), which is followed by water
quenching. In case this material is used in a strongly corrosive environment, annealing should be done at 1121°C (2050°F). This alloy cannot be hardened by heat treatment.
Threaded 45 Degree Elbow Introduction
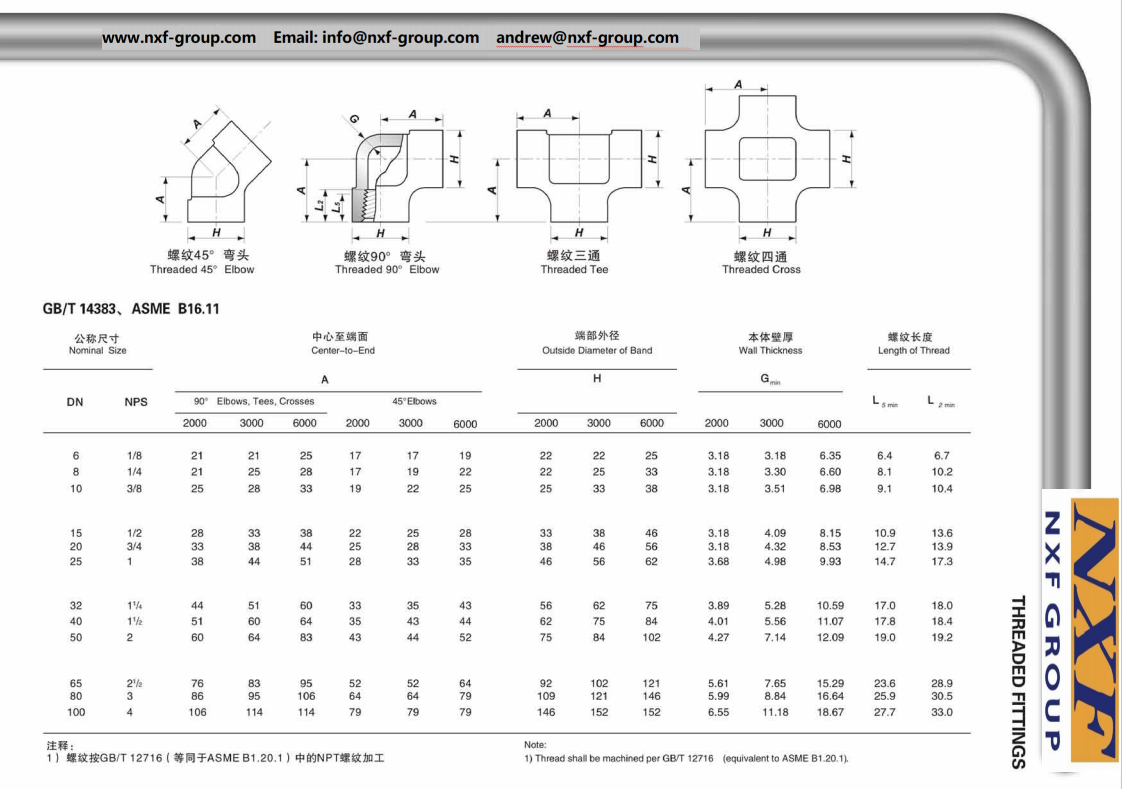
Threaded 45 Degree Elbow Drawing
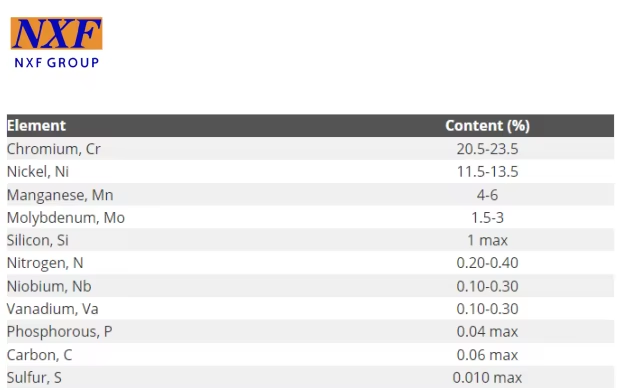
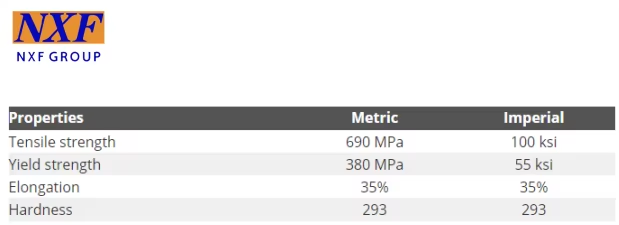
XM-19 Chemical Composition And Mechanical Properties
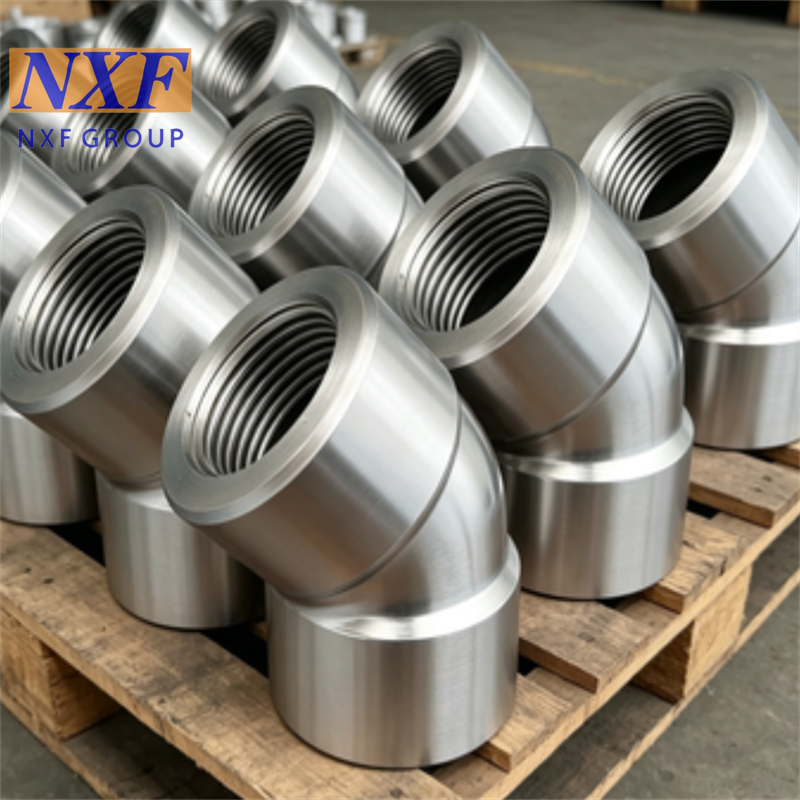
Product Image



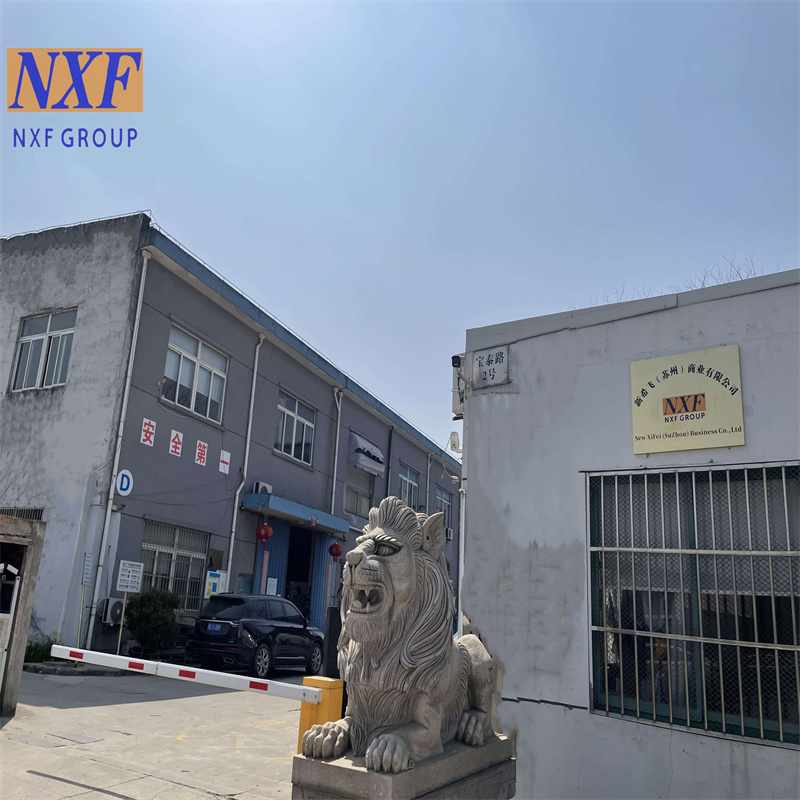
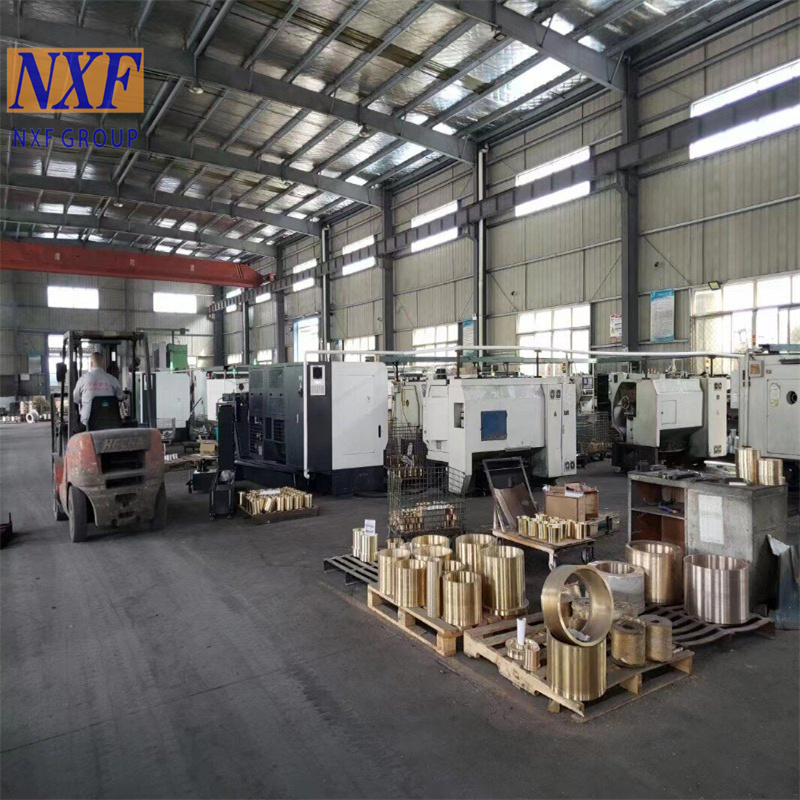
Our Advantages
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
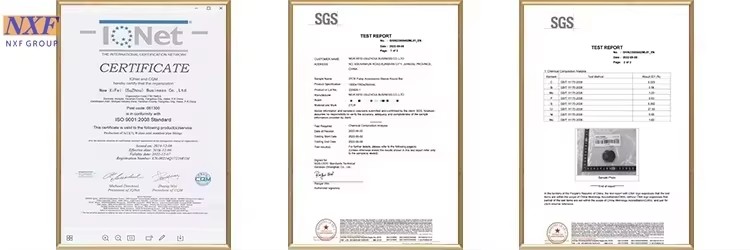
4.We have excellent quality certificate system and trademark certificat
providedbyAlibabaInternational Station,aswellas remotetechnical guidanceandservices.
6.Wehaveawell-establishedlogistics support systemthat cansaveyoubothtimeandmoney,
providingyouwithaone-stopservice.
Threaded 45 Degree Elbow Produce Processing

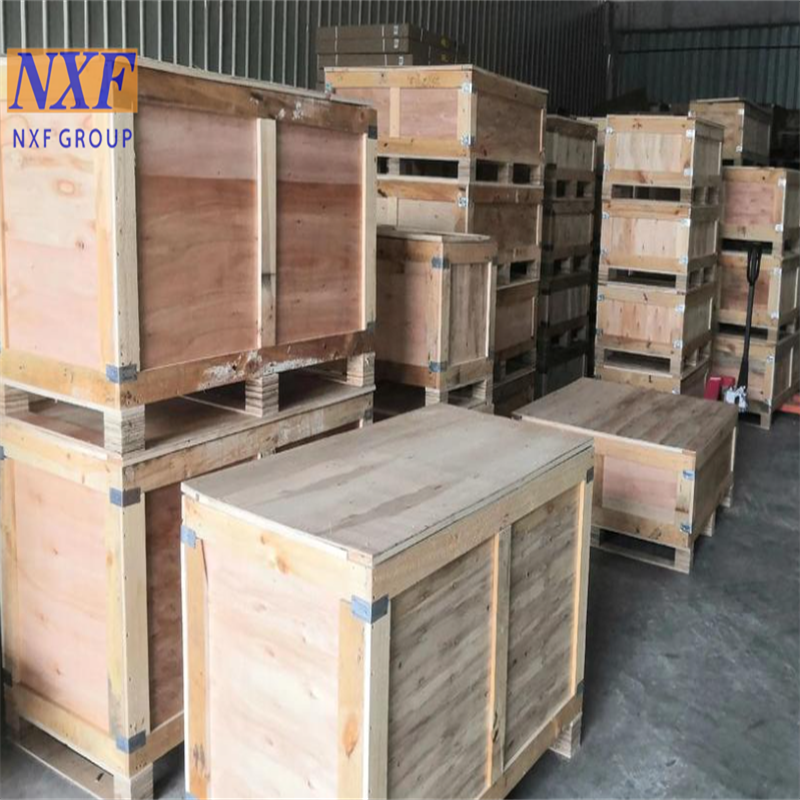


Established in 1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolute customer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management and Craftsmanship."
Our advantage as follow:
1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.

1. who are we? We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid
East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern
Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2.how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material)
We have our own factories, quality can be controlled seriously.
We Specialize in manufacturing about 21 years.
We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
LanguageSpoken:English,Chinese,Spanish,Russian