

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
NXF UNS K02600 A36/A106 OD DN15-1200 Pressure 3000-9000lb Carbon Steel Fitting Socket Welding Straight/Reducer Tee
UNS K02600 A36 Carbon steel Introduction
Machinability
Carbon steel grade UNS K02600 S235JR A36 has excellent machinability characteristics that are superior to most high-alloy steels and austenitic stainless steels; it exhibits stable cutting performance, low work hardening tendency, and good chip breaking performance under conventional processing conditions. It is recommended that standard high-speed steel or uncoated/coated carbide tooling be used, and conventional cutting speeds and feeds can be applied to achieve efficient processing.
Forming
Carbon steel grade UNS K02600 S235JR A36 can be formed using all conventional cold and hot forming methods widely applied for low-carbon structural steels. It has excellent ductility, which allows it to complete cold bending, stamping, roll forming and other cold forming processes without additional preheating at room temperature. Hot forming and forging can be done at 950-1200°C (1742-2192°F), with no strict requirements for post-forming cooling methods under general working conditions.
Welding
Welding of carbon steel grade UNS K02600 S235JR A36 can be performed using all traditional fusion welding processes, including SMAW, GMAW, SAW, GTAW and other common welding methods. Recommended filler metal should match the base material strength, commonly used grades include AWS E7018, E7016 for shielded metal arc welding, and ER70S-6 for gas metal arc welding. Preheating is generally not required for thin-walled parts at room temperature; for thick-walled parts (≥25mm) or in low-temperature environments, preheating to 50-150°C is recommended to avoid cold cracks.
Heat Treatment
Final stress relief annealing process performed for welded structural parts or precision formed parts, is done at 595-650°C
(1100-1200°F), which is followed by air cooling or furnace cooling as required. Normalizing treatment to refine grain and
homogenize structure can be done at 870-925°C (1600-1700°F). This low-carbon steel cannot be hardened by conventional quenching and tempering heat treatment, and its strength is mainly adjusted by controlled rolling and cold working.
Forging Straight/Reducer Tee Introduction
Forging Straight/Reducer Tee Drawing

UNS K02600 A36 Composition And Mechanical Properties


Product Image


TEE Produce Processing
Selection: High-quality seamless steel pipes (e.g., Carbon Steel, Stainless Steel, or Alloy Steel) are selected based on project specifications. Cutting: The pipe is cut into specific lengths (pipe blanks) using mechanical or saw cutting to ensure clean,square ends.
2. Hydraulic Bulging Process
This is the core cold-forming stage for small to medium-sized tees:
Molding: The pipe blank is placed into a hydraulic mold with a T-shaped cavity.
Internal Pressure: Ultra-high pressure liquid is injected into the blank, forcing the pipe wall to expand outward.
Axial Compensation: Simultaneously, horizontal cylinders apply axial thrust to both ends, "feeding" metal into the center to
ensure the branch pipe reaches the required height and wall thickness.
3. Branch Trimming & Sizing
Opening: The enclosed top of the formed branch is removed via plasma or mechanical cutting.
Sizing: The tee undergoes a sizing process in a precision die to ensure the dimensions and the 90-degree angle meet
international standards (e.g., ASME B16.9).
4. Heat Treatment
Purpose: To eliminate internal stresses and work hardening caused by the cold forming process.
Methods: Depending on the material, processes such as Normalizing, Tempering, or Solution Annealing (for stainless steel) are performed to restore the mechanical properties and corrosion resistance.
5. Beveling & Machining
Beveling: The three ends of the tee are machined to create welding bevels (typically at a 37.5° angle) to facilitate subsequent butt-welding at the job site.
Surface Finishing: The product is shot-blasted to remove scale and may be coated with anti-corrosion oil or paint.
6. Inspection & Testing
NDT (Non-Destructive Testing): Methods like Ultrasonic Testing (UT) or Magnetic Particle Inspection (MT) are used to check for cracks or defects.
Dimensional Check: Verification of outer diameter (OD), wall thickness (WT), and center-to-end dimensions.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
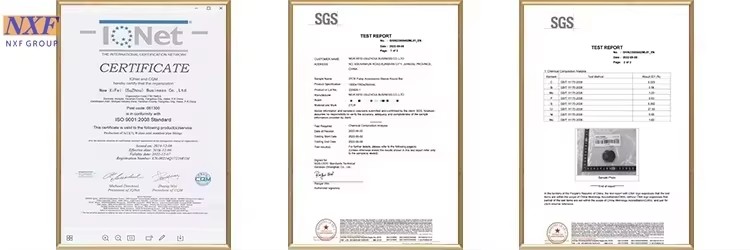
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
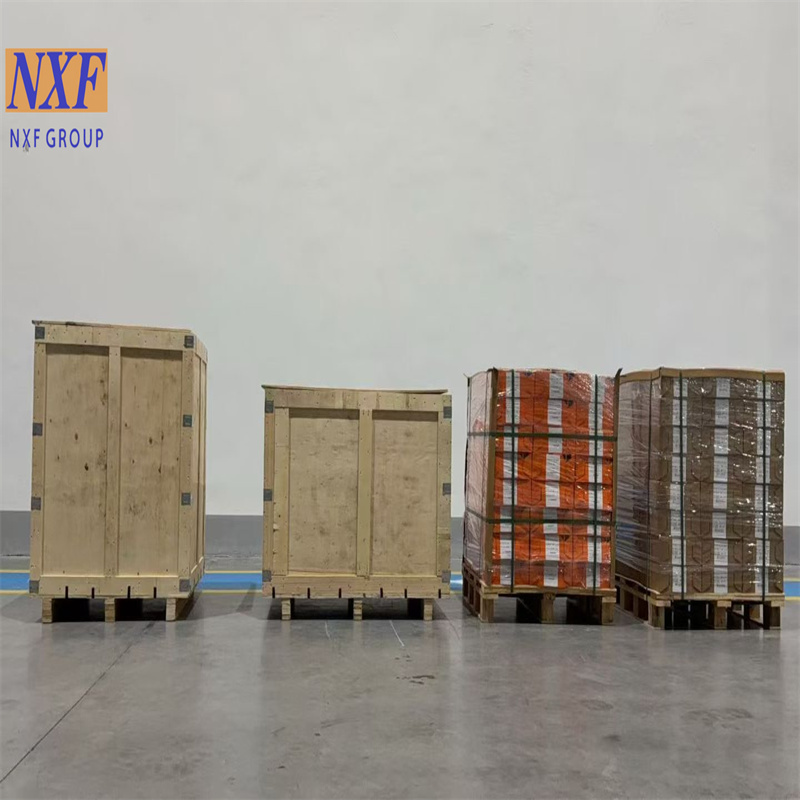
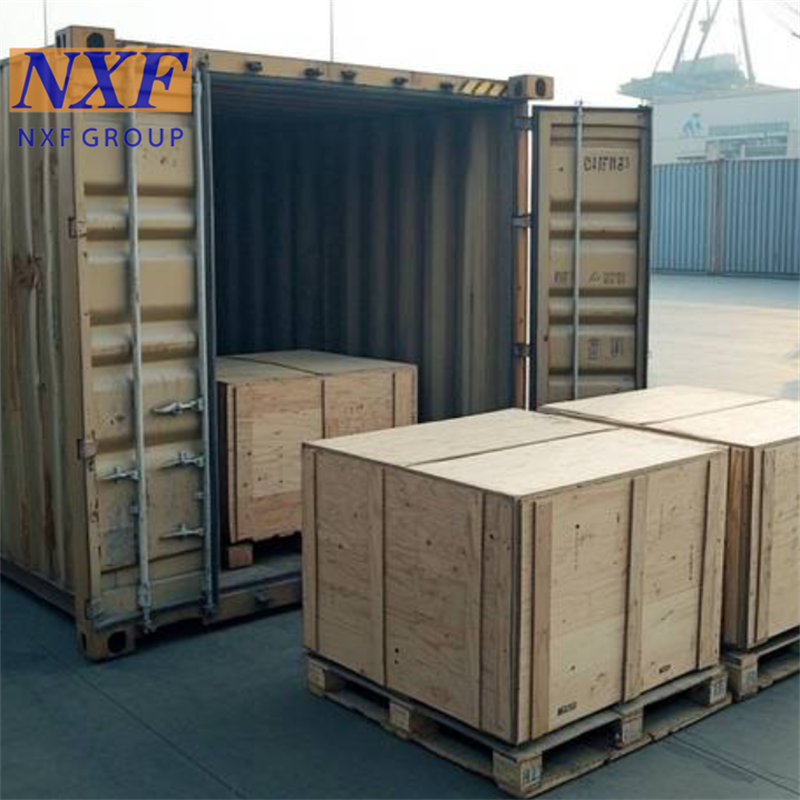
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.


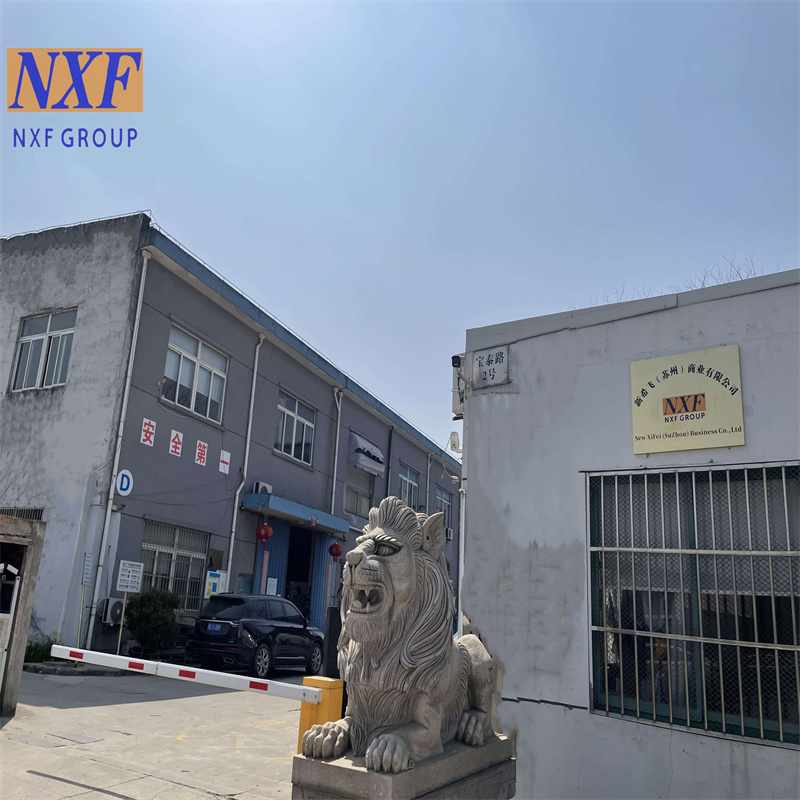
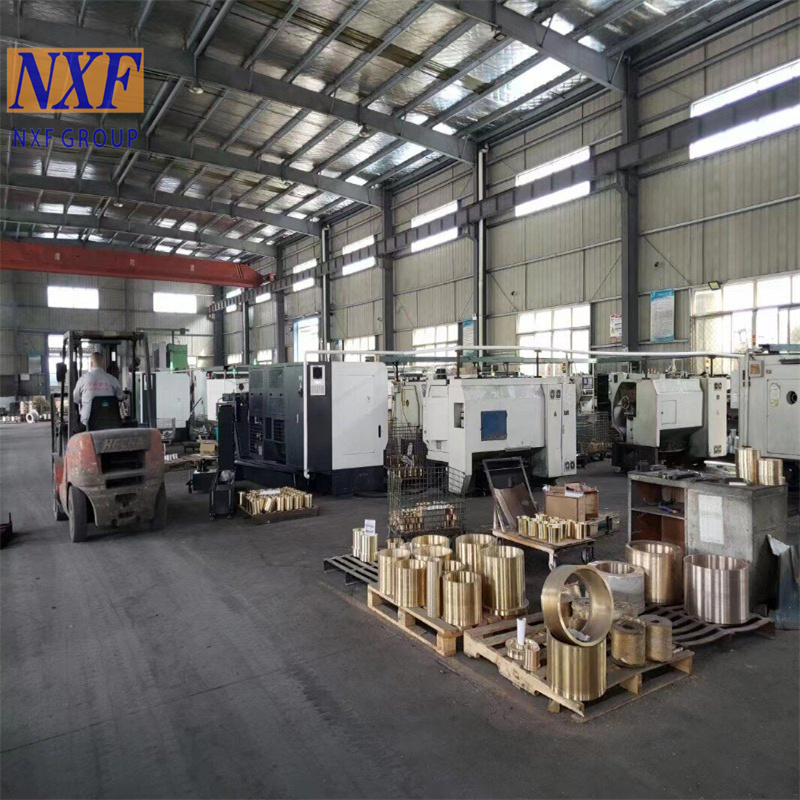
Established in 1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolute customer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management and Craftsmanship."
Our advantage as follow:
1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.

Chinese Trademark Certificate


European certificate

1. who are we? We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid
East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern
Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2.how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material)
We have our own factories, quality can be controlled seriously.
We Specialize in manufacturing about 21 years.
We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
LanguageSpoken:English,Chinese,Spanish,Russian