
NXF GROUP

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
English


NXF UNS S13800 13-8MO Out Diameter DN15-1200 Pressure Class3000-9000 Special Stainless Steel Forged Fitting Socket Weld Union
QR code
share
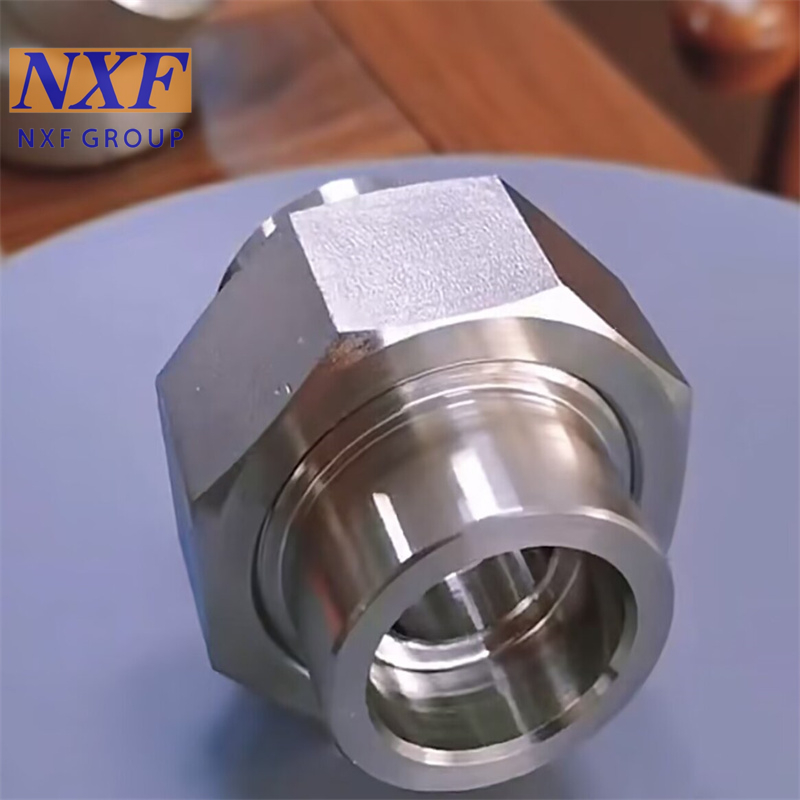
The SW union is a type of pipe connection component that is formed by casting steel bars or steel ingots and then machined. It is made of UNS S13800 stainless steel and consists of three parts: a nut, a dome head, and a flat connection.
Its connection methods include socket welding and threaded connection. Socket welding involves inserting the steel pipe into the socket hole for welding. Socket couplings come in both standard and non-standard diameters, and their structure includes components such as the socket, the socket seat, and the socket slot. The design focuses on operational convenience and leak prevention performance. The main manufacturing standards include ASME B16.11 and MSS SP 83, and they can be widely applied in various pipe diameters and scenarios such as water meters and valves.
The round steel or steel ingot is forged into shape using a die forging process, and is then precisely machined to ensure dimensional accuracy. The material is mainly stainless steel. As of 20
Its connection methods include socket welding and threaded connection. Socket welding involves inserting the steel pipe into the socket hole for welding. Socket couplings come in both standard and non-standard diameters, and their structure includes components such as the socket, the socket seat, and the socket slot. The design focuses on operational convenience and leak prevention performance. The main manufacturing standards include ASME B16.11 and MSS SP 83, and they can be widely applied in various pipe diameters and scenarios such as water meters and valves.
The round steel or steel ingot is forged into shape using a die forging process, and is then precisely machined to ensure dimensional accuracy. The material is mainly stainless steel. As of 20
DetailReview(0)
Product Description
13-8MO Introduction
13-8MO Introduction
Stainless steel grade 13-8 Mo has a high toughness and excellent resistance to stress corrosion cracking. It has been designed to handle applications where high strength, corrosion resistance, toughness, and stress resistance are essential. This is a martensitic alloy.
13-8MO Chemical Composition
13-8MO Chemical Composition
Grade 13-8 stainless steel is a high-strength, precipitation-hardening martensitic alloy known for superior toughness, corrosion resistance, and excellent transverse properties. It typically contains 12.25-13.25% Chromium, 7.5-8.5% Nickel, and 2.0-2.5% Molybdenum, often used in aerospace, nuclear, and petrochemical applications.
Introduction to common type of Socket Weld Union
Introduction to common type of Socket Weld Union
The SW union is a type of pipe connection component that is formed by casting steel bars or steel ingots and then machined. It is made of UNS S13800 stainless steel and consists of three parts: a nut, a dome head, and a flat connection.Its connection methods include socket welding and threaded connection. Socket welding involves inserting the steel pipe into the socket hole for welding. Socket couplings come in both standard and non-standard diameters, and their structure includes components such as the socket, the socket seat, and the socket slot. The design focuses on operational convenience and leak prevention performance. The main manufacturing standards include ASME B16.11 and MSS SP 83, and they can be widely applied in various pipe diameters and scenarios such as water meters and valves.The round steel or steel ingot is forged into shape using a die forging process, and is then precisely machined to ensure dimensional accuracy. The material is mainly stainless steel. As of 2025, the mainstream products comply with ASME B16.11 and MSS SP 83 standards. Socket couplings are a commonly used pipe connection component that can be easily installed and disassembled. They consist of a nut, a shoulder, and a flange. The connection methods include socket welding and threaded connection. Socket welding involves inserting the steel pipe into the socket hole for welding, hence it is called a "socket coupling", while threaded connection achieves fixation by screwing the steel pipe into the screw hole, thus it is called a "threaded coupling". This process helps control production costs, aiming to meet the strength and durability requirements of the couplings and possess leak prevention functions.
Socket Weld Union Drawing

13-8 Mo of Chemical Composition and Mechanical Properties




Our advantage as follow:
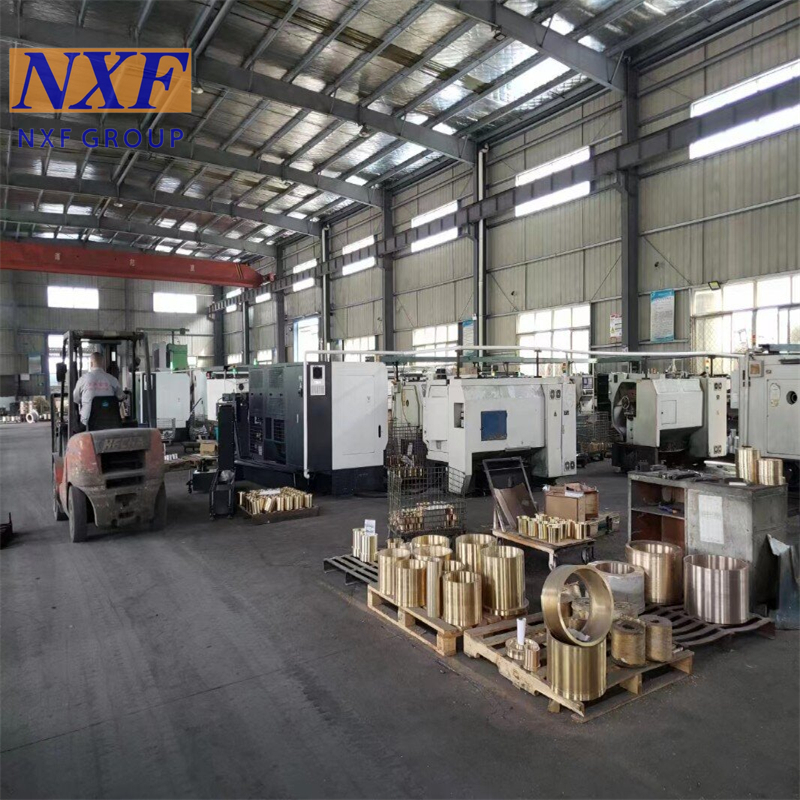
1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can giveyou the lowest price.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
4.We have excellent quality certificate system and trademark certificate
Product processing
I. Selection and Pre-treatment of Raw Materials*Raw material selection: Special stainless steel (UNS S13800) is chosen. The specific pre-treatment process for the material is determined based on the pressure and corrosive environment of the application scenario:* Cutting: Cut the raw material into appropriate blanks according to specifications* Heating: Heat the blanks either entirely or partially to enhance the plasticity of the material, facilitating subsequent processing* Surface treatment: Remove the oxide layer and oil stains to ensure processing accuracy and welding quality
II. Rough Casting Processing
*Coarse processing: The basic shape is processed using equipment such as lathes and milling machines.*Fine processing: Precise processing is carried out using CNC machines to ensure the dimensional accuracy of the sealing surfaces and socketed interfaces.
III. Key Processing Areas* Socket and Plug Interface Processing:Precisely process the inner diameter of the socket and the outer diameter of the plug to ensure that the mating clearance meets the standard requirements.Process the welding bevels inside the socket, typically in a 60° - 75° V-shaped bevel.* Sealing Surface Processing:Common sealing surface forms: flat, raised surface, concave-convex surface, mortise-slot surface.Use grinding technology to ensure the smoothness and flatness of the sealing surface to prevent leakage.
IV. Heat Treatment Process*Purpose: To eliminate processing stress, improve material mechanical properties, and enhance corrosion resistance*Common Processes:*Normalizing: To refine grains and increase material strength and toughness*Tempering: To reduce hardness and eliminate internal stress*Solution Treatment: For stainless steel materials, to enhance corrosion resistanceV. Surface Treatment and Protection*Corrosion Protection:*Stainless steel products: Perform passivation treatment to enhance corrosion resistance*Marking and Labeling:*Mark the surface of the product with information such as material, specification, pressure rating, and standard number*Common Methods: Laser marking, steel stamping markingVI. Quality Inspection and Testing*Dimensional Inspection: Use calipers, micrometers, gauges, etc. to inspect the dimensional accuracy of each part*Pressure Test: Conduct water pressure or air pressure tests to verify the sealing performance and pressure resistance*Non-destructive Testing: Use ultrasonic, magnetic particle, and penetrant testing methods to check for internal defects*Material Analysis: Confirm the material composition through spectral analysis to ensure it meets the standardsVII. Assembly and Packaging*Component Assembly: Assemble the connector body, nuts, gaskets, etc. into a complete union*Finished Product Packaging: Use anti-rust paper, plastic film, etc. for packaging to prevent damage and rust during transportation
Specification
Packing & Delivery


To better ensure the safety of your goods, professional, environmentally friendly, convenient and efficient packaging services will be provided.
Company Profile

New XiFei (SuZhou) Business Co.,Ltd is one of the leading and most respected manufacturers in China. Our products include metals,machinery, containers, construction materials, mechanical products, electrical systems, and medical accessories. Established in1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolutecustomer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management and Craftsmanship." Our advantage as follow: 1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price. 2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality. 3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
Our advantage:3S Service(Small Quantity/Short Time/Special Material)
Certification


FAQ
1. who are we?
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid East(10.00%),Eastern
Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern Europe(5.00%),Central
America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material) We have our own factories, quality can be controlled
seriously. We Specialize in manufacturing about 21 years. We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A;
Language Spoken:English,Chinese
6. Are you trading company or manufacturer ?
We are manufacturer.
7. How long is your delivery time?
Generally it is 5-10 days if the goods are in stock. or it is 15-20 days if the goods are not in stock, it is according to
quantity.
8. Do you provide samples ? is it free or extra ?
Yes, we could offer the sample for free charge but need pay the cost of freight.
9. What is your terms of payment ?
Payment<=1000USD, 100% in advance. Payment>=1000USD, 50% T/T in advance ,balance before shippment.
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid East(10.00%),Eastern
Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern Europe(5.00%),Central
America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material) We have our own factories, quality can be controlled
seriously. We Specialize in manufacturing about 21 years. We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A;
Language Spoken:English,Chinese
6. Are you trading company or manufacturer ?
We are manufacturer.
7. How long is your delivery time?
Generally it is 5-10 days if the goods are in stock. or it is 15-20 days if the goods are not in stock, it is according to
quantity.
8. Do you provide samples ? is it free or extra ?
Yes, we could offer the sample for free charge but need pay the cost of freight.
9. What is your terms of payment ?
Payment<=1000USD, 100% in advance. Payment>=1000USD, 50% T/T in advance ,balance before shippment.
Phone
+8613917160311
Whatsapp
Whatsapp
+8613917160311
Wechat
Wechat
Inquiry
Email
info@nxf-group.com
Inquiry
Inquiry
total 0 Sheet,Only 5 images can be uploaded, each less than 5m.