
Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
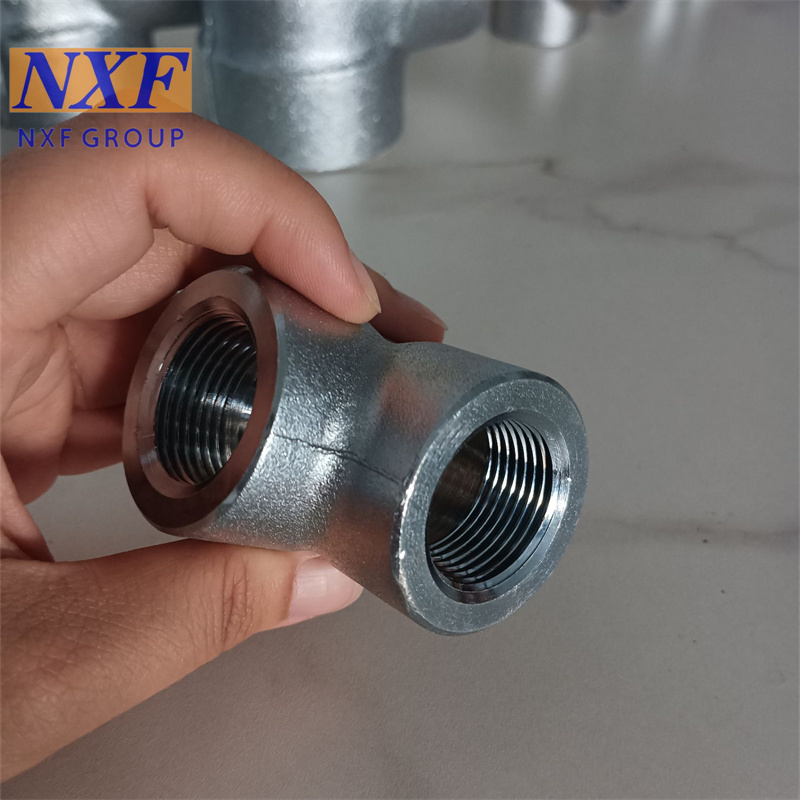
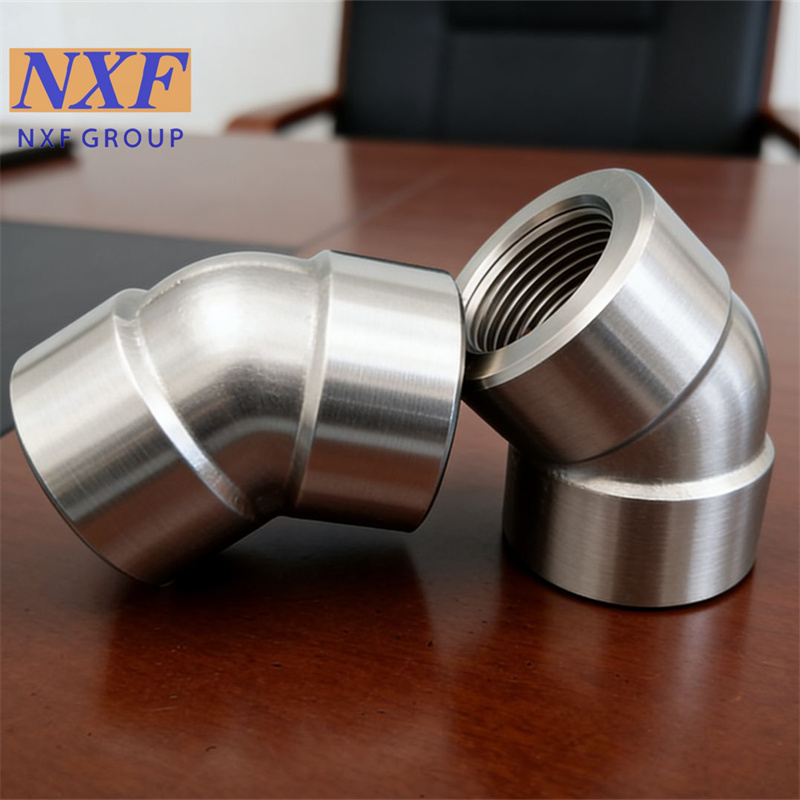
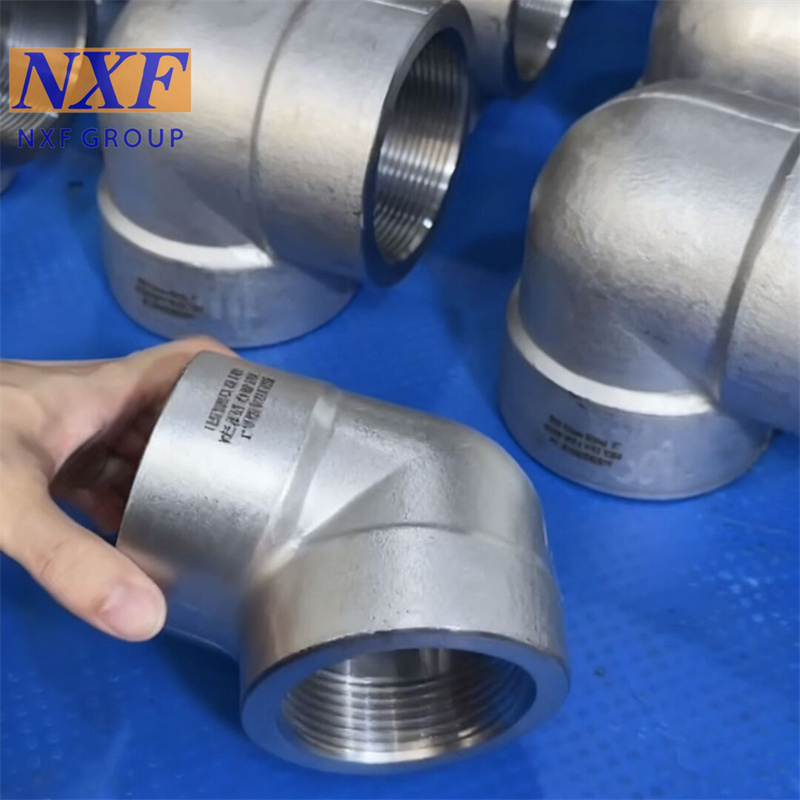
NXF ASTM A358 S38815/ZeCor-Z/ZeCor-310M DN15-1200 Class3000-9000 Special Stainless Steel Forged Fitting 90/45 Deg Thread Elbow
ZeCor-310M Introduction
Thread ElbowIntroduction
This fitting is integrally forged from ZeCor310M with dense internal structure. It features outstanding hightemperature resistance, oxidation resistance, corrosion resistance and good creep resistance, which can work reliably for a long time under severe service conditions such as high-temperature flue gas, heat treatment pipelines and high-temperature process media.
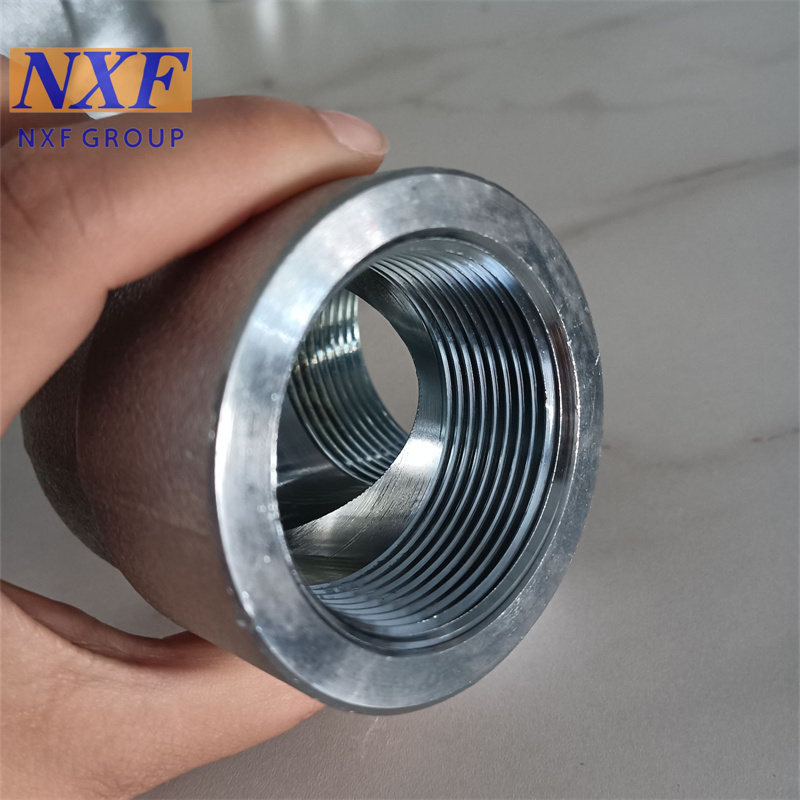
Both ends are tapered pipe threads, normally NPT threads. Sealing is realized by threaded engagement without welding. It is easy to install and convenient for later disassembly and maintenance. It covers pressure classes of 2000LB, 3000LB and 6000LB, sizes ranging from 1/8″ to 4″ (DN6-DN100). It is widely used in petrochemical, energy, metallurgy, high-temperature instrument sampling lines and high-temperature process piping systems.





Thread ElbowProduct Processing
1. Raw Material InspectionRaw material is ZeCor-310M bar stock. Verify material certificates, perform spectrum test for chemical composition and mechanical properties. Mark heat numbers for full traceability.
2. CuttingCut billets according to drawing dimensions, remove burrs and scale on cutting surfaces, reserve allowance for forging and machining.
3. Heating and Closed Die ForgingHeat billets to specified forging temperature, forge elbow blanks by closed die forging, control process parameters to achieve uniform and dense grain structure.
4. Heat TreatmentSolution treatment is carried out in accordance with dedicated ZeCor-310M procedure to release forging stress and stabilize high-temperature and corrosion resistance.
5. Shot BlastingRemove scale and forging contaminants from blank surface by shot blasting.
6. Precision MachiningCNC turning for NPT tapered threads, elbow profile and end faces. Strictly control thread form accuracy, thread length, center-to-end dimension and wall thickness tolerance to guarantee threaded sealing performance.
7. MarkingLaser marking of material, size, pressure class, heat number and standard number.
8. Finished Product InspectionDimensional check, visual inspection, hardness test, PT penetrant testing as required to detect surface defects.
9. Surface PassivationPassivation treatment to improve corrosion resistance.
10. Final Inspection & Document PreparationRecheck all test items, compile MTC, test reports and inspection records.
11. Packing and WarehousingProtective packing, classified storage with full quality documents attached.
Our NXF GROUP advantage as follow
2.Our NXF GROUP can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and size testing.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent quality certificate system and trademark certificate.
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.


We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),Eastern Asia(10.00%),Mid East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:
2.Our NXF GROUP can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and size testing.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent quality certificate system and trademark certificate.
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian