
NXF GROUP

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
English
NXF UNS NO7718/2.4668/NiCr19NbMo/alloy 718 DN15-1200 Class3000-9000 Nickel Alloy Forged Fitting Threaded Latrolet/Elbolet
2026-09-20 20:12 NXF GROUP
3
Product Description
Alloy 718 Introduction.
Alloy 718/2.4668 is a nickel-chromium iron alloy with niobium and molybdenum and low contained aluminum and tnum. Excellent mechanical properties in lower temperatures. Excellent corrosion resistance at high and low temperatures
Inconel 718 is a nickel based super alloy that is well suited for applications requiring high strength in temperature ranges from cryogenic up to 1400°F. Inconel 718 also exhibits excellent tensile and impact strength.
Inconel 718 is a nickel based super alloy that is well suited for applications requiring high strength in temperature ranges from cryogenic up to 1400°F. Inconel 718 also exhibits excellent tensile and impact strength.
Threaded Latrolet/Elbolet Introduction
1.Product Definition:
Threaded Latrolet and Threaded Elbolet are forged integral branch reinforcement fittings manufactured to MSS SP-97 standard. Threaded Latrolet is welded on straight pipe for 45° angled threaded branch connection. Threaded Elbolet is mounted on 90° elbow to create threaded outlet. The branch end is machined with standard NPT thread for threaded pipe connection.
2.Structural Features:
One-piece forged construction delivers dense metallurgical structure. The curved saddle base fits tightly against the outer
surface of host pipe or elbow. Internal NPT threads are precisely machined, ensuring tight sealing. No extra reinforcing plate is required, which avoids weak points from patch welding.
3.Applicable Working Conditions:
They are widely used in petroleum, chemical, power and natural gas piping systems for medium and high pressure service. Available materials include carbon steel, stainless steel, alloy steel and Inconel 718. Common pressure classes are 3000LB and 6000LB, ideal for sampling, venting and instrument tapping points.
4.Installation Method:
The saddle base is welded onto the outer wall of the main pipe or elbow by continuous fillet weld. The threaded outlet directly mates with threaded pipes or instrumentation components. The integral reinforcement reduces stress concentration at the pipe opening and lowers the risk of cracking. Field installation is fast and convenient.
5.Core Difference between Latrolet and Elbolet:
Threaded Latrolet has a curved base matching straight pipe, providing a 45° threaded branch from straight pipe runs. Threaded Elbolet features a special curved profile to perfectly fit the outer surface of a 90° elbow; it can only be installed on elbows rather than straight pipe sections.
6.Quality Control & Testing:
All fittings undergo strict inspection including dimensional verification, visual check, liquid penetrant testing (PT) and
ultrasonic testing (UT). Thread gauge inspection is performed to guarantee thread accuracy. Material test certificates are
supplied with finished goods for traceability.
Threaded Latrolet and Threaded Elbolet are forged integral branch reinforcement fittings manufactured to MSS SP-97 standard. Threaded Latrolet is welded on straight pipe for 45° angled threaded branch connection. Threaded Elbolet is mounted on 90° elbow to create threaded outlet. The branch end is machined with standard NPT thread for threaded pipe connection.
2.Structural Features:
One-piece forged construction delivers dense metallurgical structure. The curved saddle base fits tightly against the outer
surface of host pipe or elbow. Internal NPT threads are precisely machined, ensuring tight sealing. No extra reinforcing plate is required, which avoids weak points from patch welding.
3.Applicable Working Conditions:
They are widely used in petroleum, chemical, power and natural gas piping systems for medium and high pressure service. Available materials include carbon steel, stainless steel, alloy steel and Inconel 718. Common pressure classes are 3000LB and 6000LB, ideal for sampling, venting and instrument tapping points.
4.Installation Method:
The saddle base is welded onto the outer wall of the main pipe or elbow by continuous fillet weld. The threaded outlet directly mates with threaded pipes or instrumentation components. The integral reinforcement reduces stress concentration at the pipe opening and lowers the risk of cracking. Field installation is fast and convenient.
5.Core Difference between Latrolet and Elbolet:
Threaded Latrolet has a curved base matching straight pipe, providing a 45° threaded branch from straight pipe runs. Threaded Elbolet features a special curved profile to perfectly fit the outer surface of a 90° elbow; it can only be installed on elbows rather than straight pipe sections.
6.Quality Control & Testing:
All fittings undergo strict inspection including dimensional verification, visual check, liquid penetrant testing (PT) and
ultrasonic testing (UT). Thread gauge inspection is performed to guarantee thread accuracy. Material test certificates are
supplied with finished goods for traceability.
Threaded Latrolet/Elbolet Drawing

Alloy 718 Chemical composition and mechanical properties

Factory and Product Pictures
Threaded Latrolet/Elbolet Factory and Product Pictures


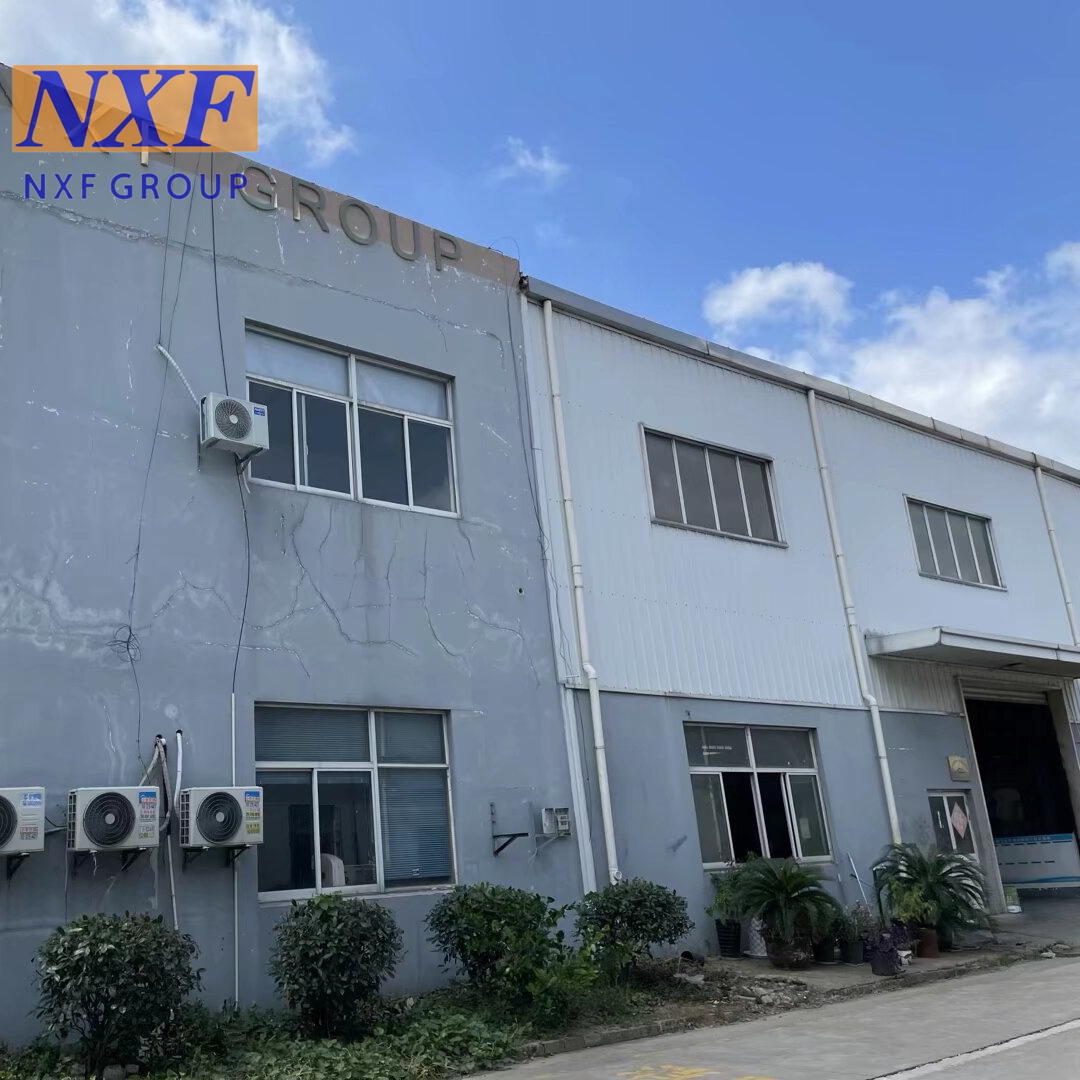
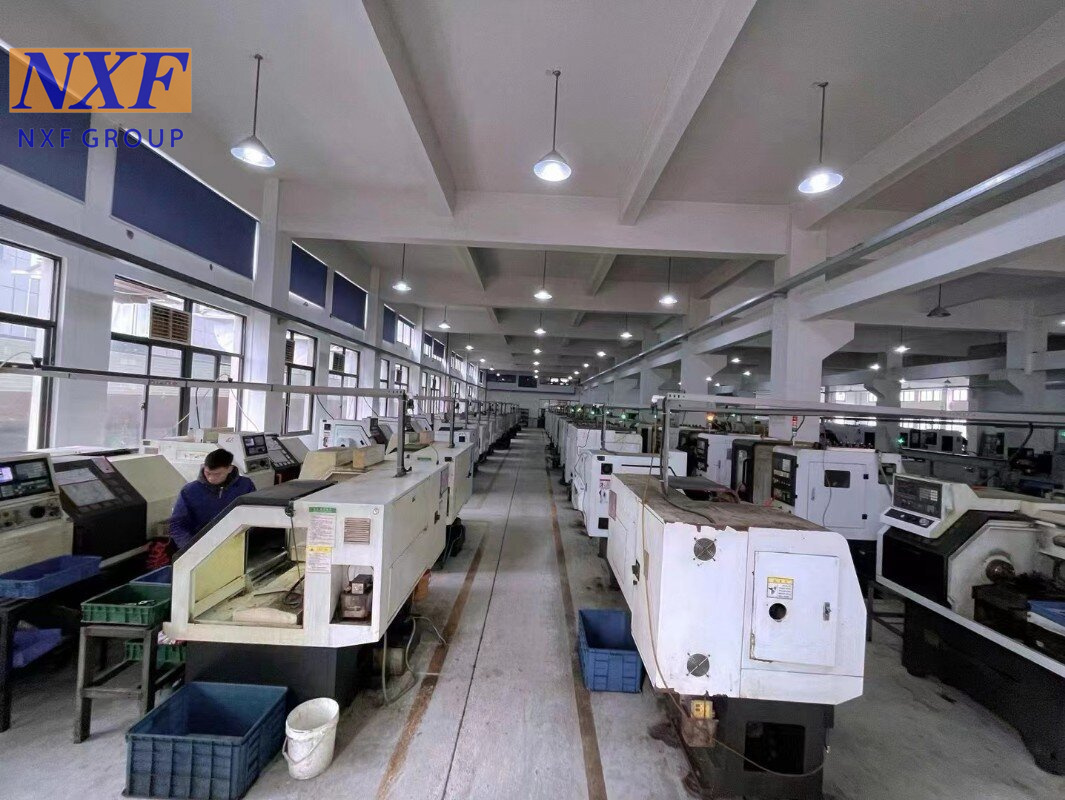
Alloy 718 PMI spectral testing proves

Customer visit to the factory video
718 Threaded Latrolet/Elbolet Produce Processing
1. Raw Material Inspection:
All raw steel bars and forging blanks are strictly inspected before production. Chemical composition, mechanical properties and internal quality are verified in accordance with MSS SP-97 and relevant material standards. Unqualified materials are rejected to ensure overall product reliability.
2. Hot Forging and Blank Forming:
Qualified raw materials are heated and precision forged into integral Latrolet and Elbolet blanks. The forging process eliminates internal porosity, refines grain structure, and improves mechanical strength, toughness and pressure resistance of the branch fittings.
3. Heat Treatment:
Forged blanks undergo standardized heat treatment including normalizing, quenching or aging according to material requirements. This process stabilizes the metallographic structure, relieves forging stress, and ensures stable hardness and high-pressure performance.
4. Precision CNC Machining:
The blank is processed by CNC turning and milling. The saddle curved surface, outer contour, inner hole and welding bevel are precisely machined to fit the main pipe or elbow perfectly. All dimensions strictly follow standard tolerance requirements.
5. NPT Thread Machining and Calibration:
Standard NPT internal threads are precisely cut on the branch outlet. Each thread is inspected with professional thread gauges to ensure accurate taper, smooth tooth surface and reliable self-sealing performance for threaded connection.
6. Non-Destructive Testing and Quality Inspection:
All finished products undergo visual inspection, dimensional inspection, PT and UT non-destructive testing. Surface cracks, internal defects and dimensional errors are fully checked to meet industrial high-pressure piping standards.
7. Surface Treatment and Packaging:
Qualified fittings are cleaned, polished and rust-proof treated. Product marks such as size material grade and heat number are engraved. Finally, finished products are packed with protective materials and accompanied by complete inspection documents for delivery.
Our NXF GROUP advantage as follow
1.Our NXF GROUP have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price based on best quality.
2.Our NXF GROUP can strictly control the quality. We have production,quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and sizetesting.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.
Packing & Delivery
Packing


Delivery

Company Profile

New XiFei (SuZhou) Business Co.,Ltd is one of the leading and most respected manufacturers in China. Our products
includemetals,machinery, containers, construction materials, mechanical products, electrical systems, and medical
accessories.Establishedin1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolutecustomer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management andCraftsmanship." Our advantage:3S Service(Small Quantity/Short Time/Special Material).
includemetals,machinery, containers, construction materials, mechanical products, electrical systems, and medical
accessories.Establishedin1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolutecustomer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management andCraftsmanship." Our advantage:3S Service(Small Quantity/Short Time/Special Material).
Specification


FAQ
1. who are we?
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),South America(10.00%),Eastern Europe(10.00%),Mid East(10.00%),Eastern Asia(10.00%),Southeast Asia(5.00%),Africa(5.00%),Central America(5.00%),Northern Europe(5.00%),North America(5.00%),Domestic Market(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
1.Our NXF GROUP have our own factory, and we can control the cost by
producing by ourselves. We have a great advantage in price and can give you the lowest price based on best quality.
2.Our NXF GROUP can strictly control the quality. We have production,quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and size testing.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian
We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),South America(10.00%),Eastern Europe(10.00%),Mid East(10.00%),Eastern Asia(10.00%),Southeast Asia(5.00%),Africa(5.00%),Central America(5.00%),Northern Europe(5.00%),North America(5.00%),Domestic Market(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
1.Our NXF GROUP have our own factory, and we can control the cost by
producing by ourselves. We have a great advantage in price and can give you the lowest price based on best quality.
2.Our NXF GROUP can strictly control the quality. We have production,quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and size testing.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian
声明:此篇为NXF GROUP原创文章,转载请标明出处链接: https://www.nxf-group.com/h-nd-2358.html
Phone
+8613917160311
Whatsapp
Whatsapp
+8613917160311
Wechat
Wechat
Inquiry
Email
info@nxf-group.com
Inquiry
Inquiry