

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com
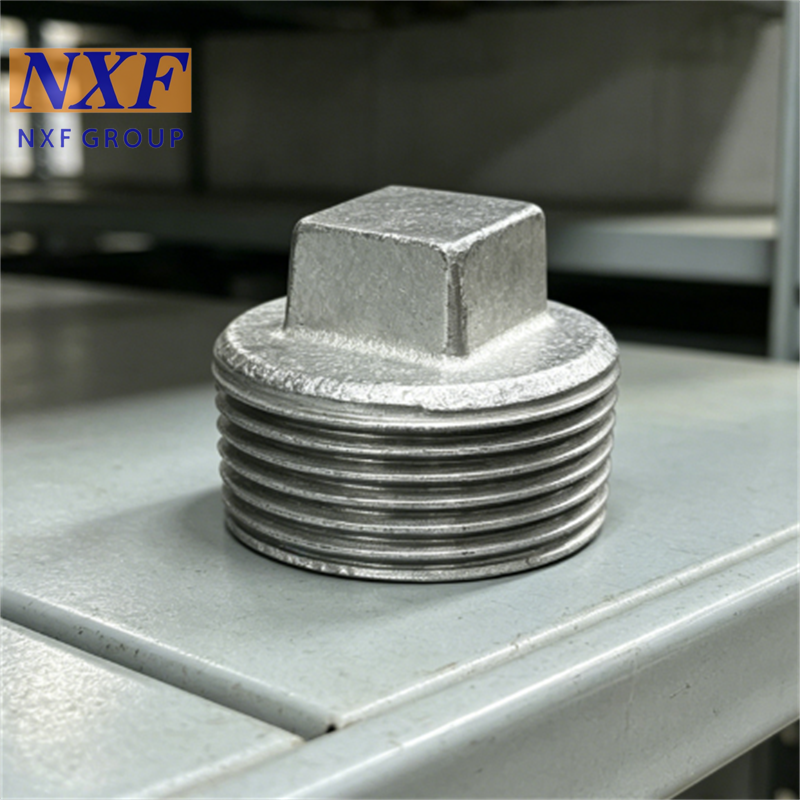
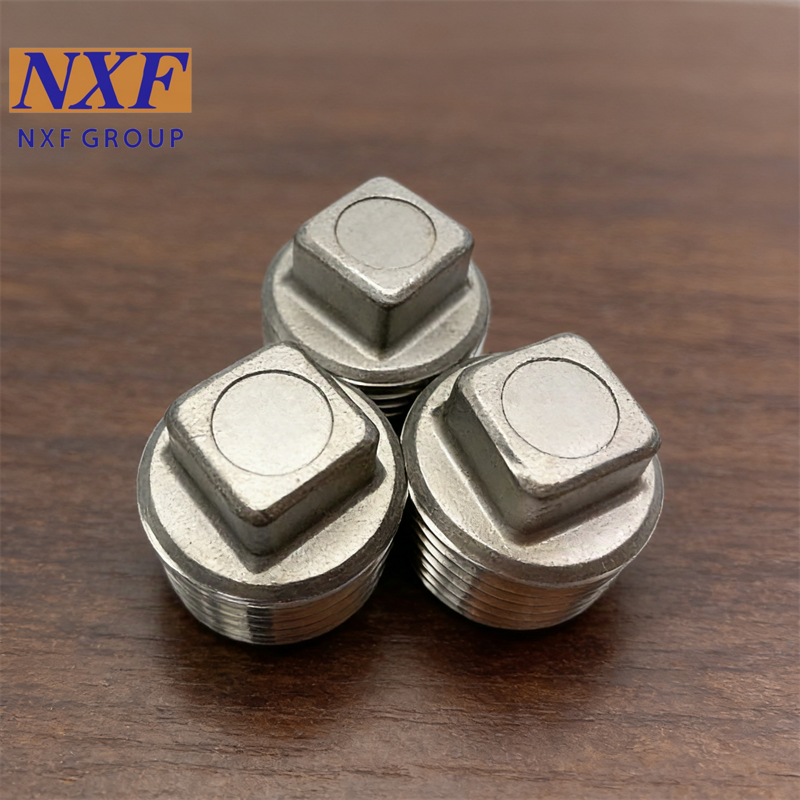
NXF UNS S30400 ASTM 304/JIS 304/EN 1.4301 DN6-1200 Class3000-9000 Stainless Steel 304 Forged Fitting Threaded Square Head Plug
Stainless Steel 304 Introduction
commonly referred to as "18/8" because of its nominal composition of 18% chromium and 8% nickel, with the balance being iron plus small amounts of carbon, manganese, and silicon. It offers an excellent balance of corrosion resistance, formability, and weldability, making it the default choice for general-purpose applications. In its annealed condition, it is essentially non-magnetic and maintains good toughness across a wide temperature range, including cryogenic service.
Typical uses include kitchen equipment, food and beverage processing, architectural panels, chemical containers, water piping, automotive trim, and fasteners. It performs well in atmospheric, fresh-water, and mildly chemical environments.
Its main limitation is susceptibility to chloride-induced pitting and crevice corrosion, so it is not recommended for marine,
coastal, or high-salt service — for those environments.
Threaded Square Head PlugIntroduction
1.Structural Characteristics
Threaded square head plug is a pipe fitting with external thread and square head. The squ e head on the top allows clamping by spanner for easy tightening and removal. Its threaded section can be screwed into the internal thread of pipe or equipment port to seal the opening. Compact structure, no extra welding required.
2.Installation Features
Installation is simple and fast. Directly screw the plug into the threaded port with a wrench. No welding or special tooling is needed. It can be repeatedly disassembled for maintenance, inspection or fluid sampling of pipeline systems.
3.Application Range
It is widely used to block unused openings on pressure vessels, pumps, valves and piping systems. Suitable for oil, gas, water and general chemical medium pipelines. Commonly applied for temporary or permanent sealing in low and medium pressure working conditions.
4.Sealing Performance & Restrictions
Sealing relies on thread fit and optional sealing compound or PTFE tape. It works well under stable pressure. Not recommended for strong vibration, sharp pressure fluctuation or highly corrosive media, which may cause thread loosening and leakage.
5.Standards & Material Selection
Common manufacturing standards include ASME B16.11. Available materials cover carbon steel, stainless steel and alloy steel. Thread types can be NPT, BSPT and BSPP. Surface treatment such as galvanizing can be added for rust prevention.



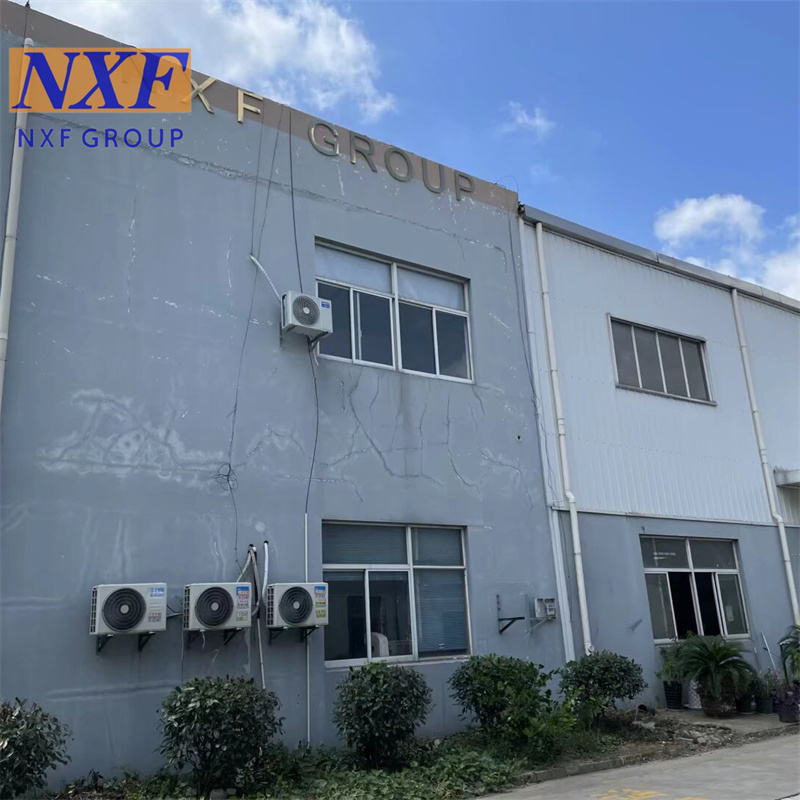
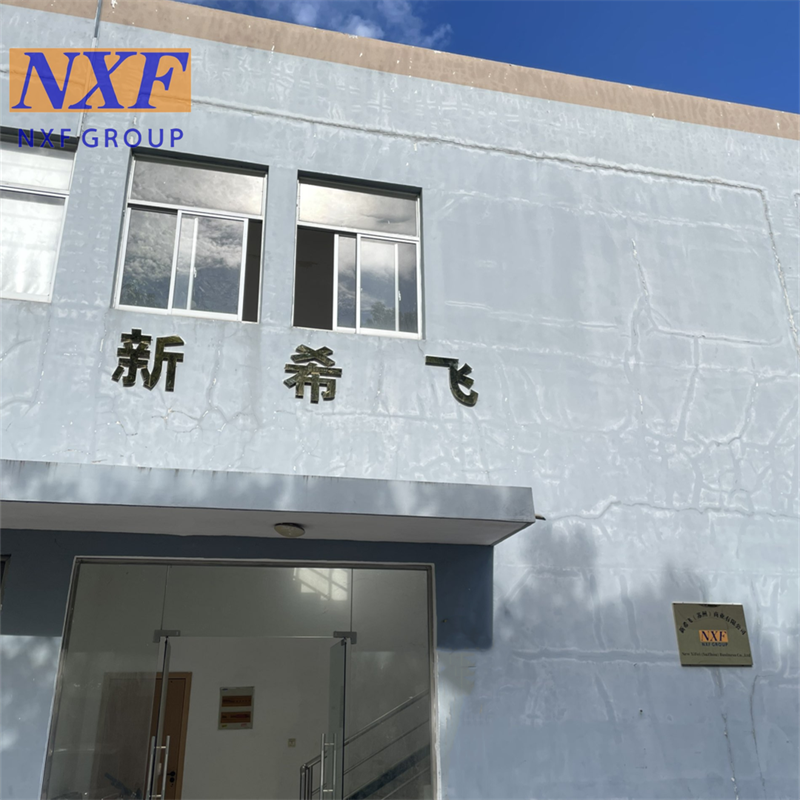
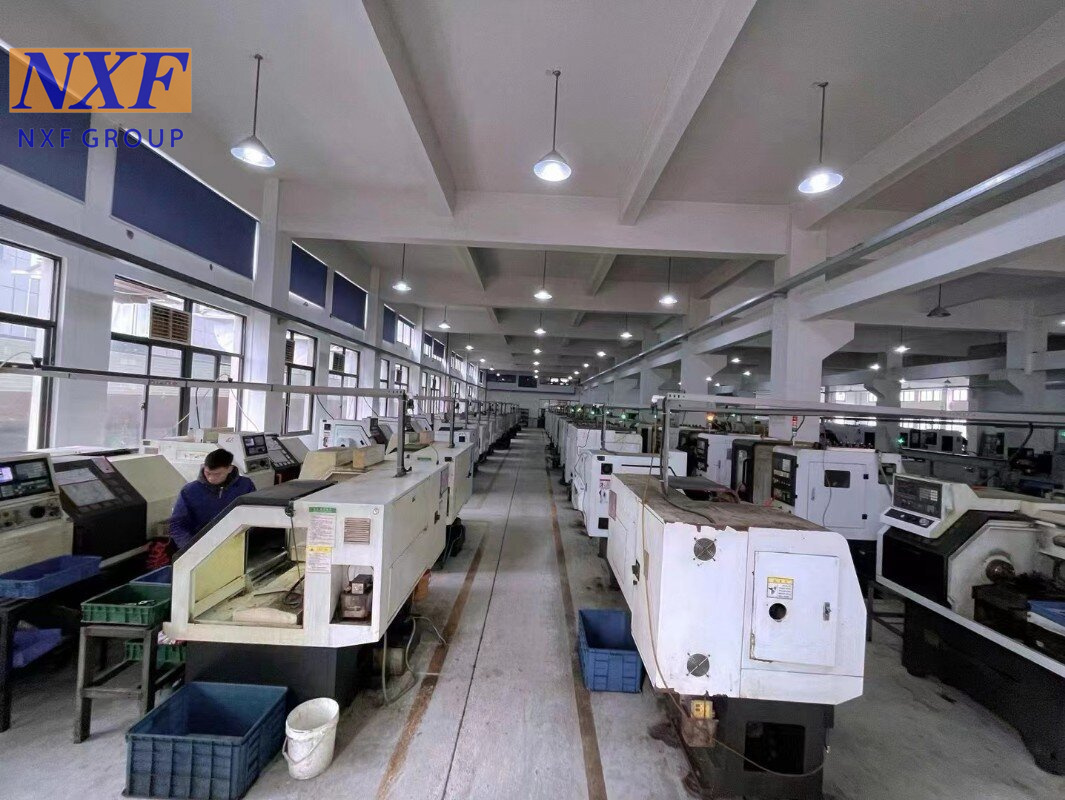

Customer visit to the factory video
Threaded Square Head Plug Produce Processing
1..Raw Material Inspection and Cutting
Inspect raw bar stock to confirm chemical composition and mechanical properties conform to required standards. Check surface for cracks, pits and other defects. Cut bars into blanks with appropriate machining allowance according to drawing dimensions.
2.Hot Forging / Heading Forming
Heat the cut blank to the target forming temperature. Upset one end to form the square head and rough outer contour of the plug. Strictly control heating temperature and forming force to prevent internal flaws and incomplete square head shaping.
3.Heat Treatment
Perform normalizing or tempering after forming. Eliminate forming residual stress, adjust hardness and improve material toughness. Avoid deformation during subsequent machining and enhance the mechanical strength of finished plugs.
4.Precision Machining
Use CNC lathe to machine outer cylindrical surface and external threads. Mill four sides of the square head to meet size and flatness requirements. Remove sharp edges and ensure all tolerances comply with drawing specifications.
5.Surface Treatment
Clean machining chips and burrs. Carry out shot blasting to remove scale. Conduct galvanizing, blackening or anti-rust oil coating as per customer requirements to achieve corrosion resistance.
6.Final Inspection and Marking
Conduct thread gauge test, dimensional measurement and visual inspection. Verify thread tightness and surface integrity. Mark material grade, heat number and standard on qualified parts, then pack for shipment.
Our NXF GROUP advantage as follow
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.


includemetals,machinery, containers, construction materials, mechanical products, electrical systems, and medical
accessories.Establishedin1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolutecustomer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management andCraftsmanship." Our advantage:3S Service(Small Quantity/Short Time/Special Material).


We are based in Jiangsu, China, start from 2021,sell to South Asia(30.00%),South America(10.00%),Eastern Europe(10.00%),Mid East(10.00%),Eastern Asia(10.00%),Southeast Asia(5.00%),Africa(5.00%),Central America(5.00%),Northern Europe(5.00%),North America(5.00%),Domestic Market(5.00%). There are total about 101-200 people in our office.
2. how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
2.Our NXF GROUP can strictly control the quality. We have production,quality inspection, warehousing and other departments to coordinate and control the quality,Such as PMI and size testing.
3.Our NXF GROUP biggest advantage is 3S service. Small quantity, short time, special materials.
4.Our NXF GROUP have excellent qualitycertificate system and trademark certificate
5.Our NXF GROUP have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by AlibabaInternational Station, as well as remote technical guidance and services.
6.Our NXF GROUP have a well-established logistics support system that can save you both time and money, providing you with aone-stop service.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
Language Spoken:English,Chinese,Spanish,Russian