

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com


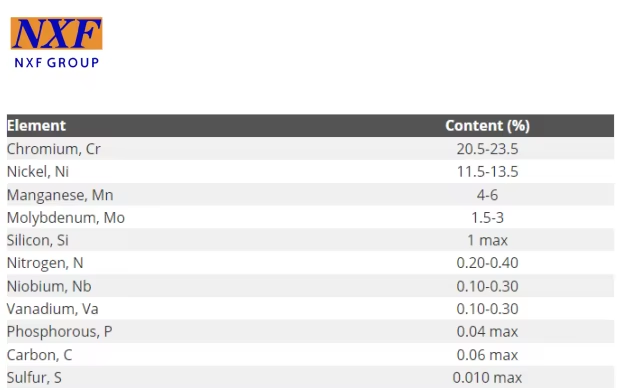
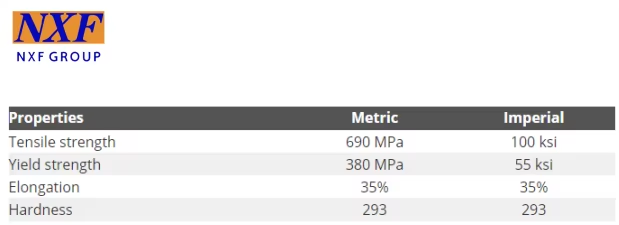
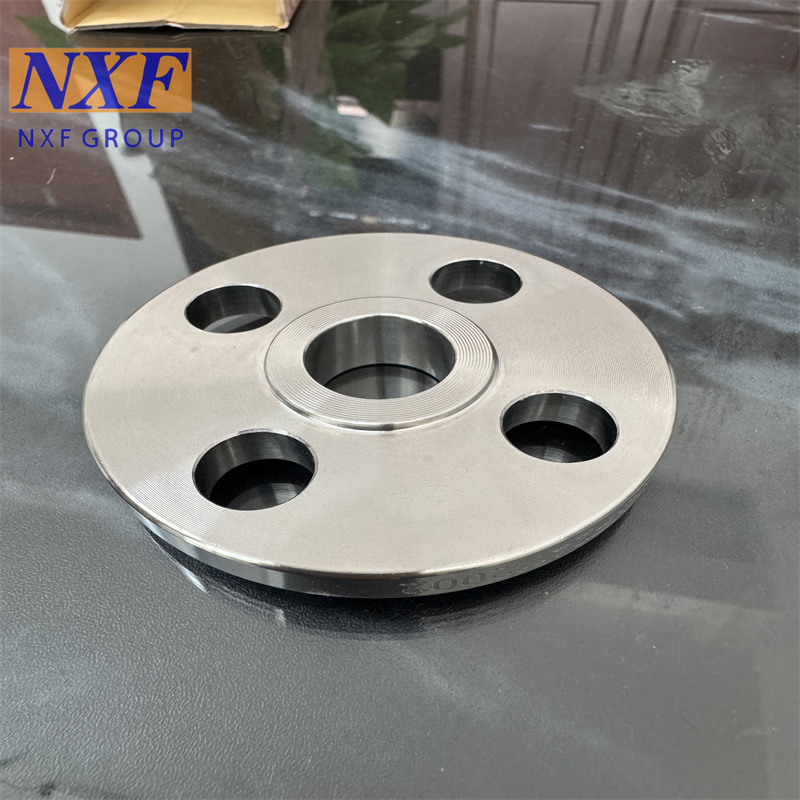
NXF UNS S20910 XM-19 Diameter DN15-1200 Pressure 150-1500lb Special Stainless Steel Forged Slip on Flanges
Slip On Welding Flanges, commonly abbreviated as SO Flanges, are one of the most universal and cost-effective pipe flange types widely applied in global industrial pipeline systems. Featuring a short straight hub and larger inner bore, this flange is designed to slide directly over the outer diameter of connecting pipes, and permanently fixed by double fillet welding on both internal and external sides.
magneticpermeability of this alloy allows it to be used as a material for medical implants.
Machinability
Stainless steel grade UNS S20910 XM-19 has machinability characteristics that are similar to other austenitic stainless
steels;however it requires slower speeds, more power, and higher rigidity due to its high work hardening rate. It is recommended that coated carbide tooling be used.
Forming
Stainless steel grade UNS S20910 XM-19 can be formed using the same methods applied for other austenitic stainless steels. More power for forming and forging is needed for this alloy. Forging can be done at 1177-1204°C (2150-2200°F).
Welding
Welding of stainless steel grade UNS S20910 XM-19 can be performed using traditional joining processes. Recommended filler metal should be UNS S20910 XM-19 (AWS E/ER209).
Caution should be taken while using autogenous, high power density joining processes such as EB or laser welding, due to low FN potential and severe outgassing possibility.
Heat Treatment
Final annealing process performed for several of the applications, is done at 1065°C (1950°F), which is followed by water
quenching. In case this material is used in a strongly corrosive environment, annealing should be done at 1121°C (2050°F). This alloy cannot be hardened by heat treatment.





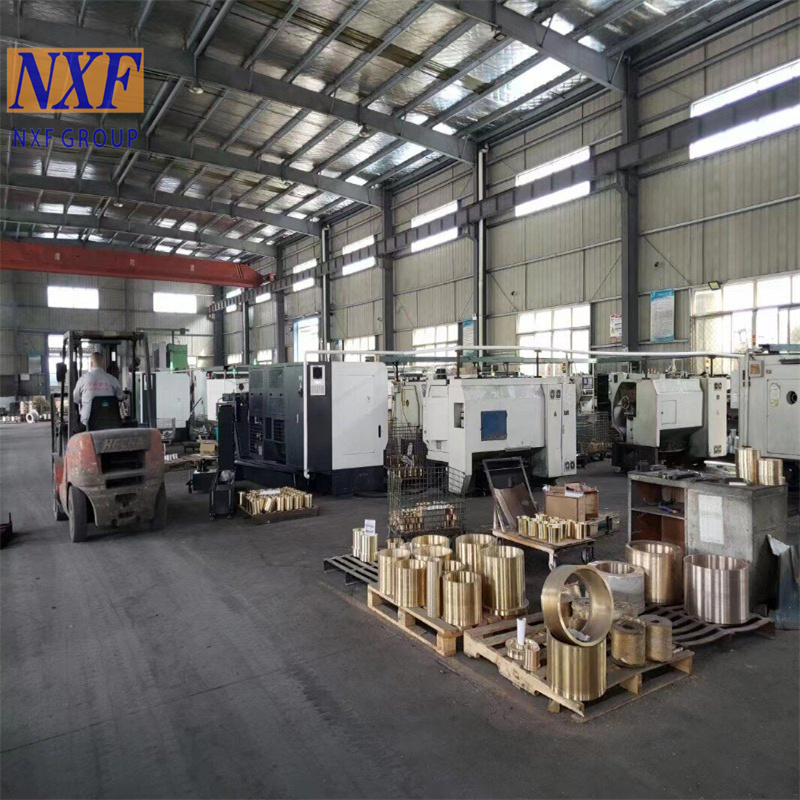
Product processing
1. Raw Material CuttingSelect qualified solid steel billets and cut them into blanks of the required weight and size using high-precision band saw cutting equipment.Each blank is pre-loaded with appropriate machining and forging shrinkage allowance. After cutting, burrs and sharp edges on the blank surface are initially removed.
2. Hot Forging ProcessHeating The cut blanks are fed into a heating furnace and heated to the standard forging temperature range. A constant temperature is maintained to ensure uniform heating inside and outside the blank, laying a good foundation for stable forming.Forging The heated blanks are forged using a hydraulic press or forging hammer. The basic outline of the sliding flange is formed, including the flange outer plate, inner bore, and short straight hub structure.During forging, the internal metal grain structure is refined, improving the overall structural strength and mechanical properties of the flange.Natural Cooling The forged blanks are placed in air and slowly cooled to room temperature to avoid rapid cooling that could lead to internal cracks and excessive residual stress
.3. Heat TreatmentHeat treatment is performed on the forged billet to eliminate internal stresses generated during forging, stabilize the overall structure, and improve machinability.The billet is heated to a specified temperature, held for a sufficient time, and then cooled according to standard procedures. This process optimizes mechanical properties and reduces the risk of deformation during subsequent precision machining.
4. Precision CNC MachiningRough Turning The forged billet is machined on a CNC lathe. Rough turning is performed on the flange outer diameter, flange thickness, inner bore, and hub surface, with uniform finishing allowances left on all surfaces.Finish Turning Precision finishing is performed on all flange components. The flange sealing surface, hub profile, and inner bore dimensions are machined to meet standard dimensional tolerances. Strict control is maintained over the surface flatness and smoothness of the sealing surfaces.Bolt Hole Machining Uniformly distributed circumferential bolt holes are drilled using CNC drilling equipment according to standard specifications for bolt diameter, number of holes, and hole diameter. Strict accuracy in bolt hole position, spacing, and perpendicularity is ensured.
5. Surface Treatment and CleaningAll machining residues, cutting debris, scale, and oil stains on the flange surface are removed by shot blasting.All sharp edges are chamfered and polished to prevent scratches and potential damage during assembly and transportation.
6. Quality InspectionA comprehensive quality inspection is performed on the finished flanges.Measure the overall dimensions of the flange, inner bore dimensions, outer diameter, thickness, and bolt hole parameters.Inspect for surface defects, eliminating cracks, pits, and other surface defects.Perform hardness testing and visual inspection on the finished products.All non-conforming products are rejected and reworked individually.
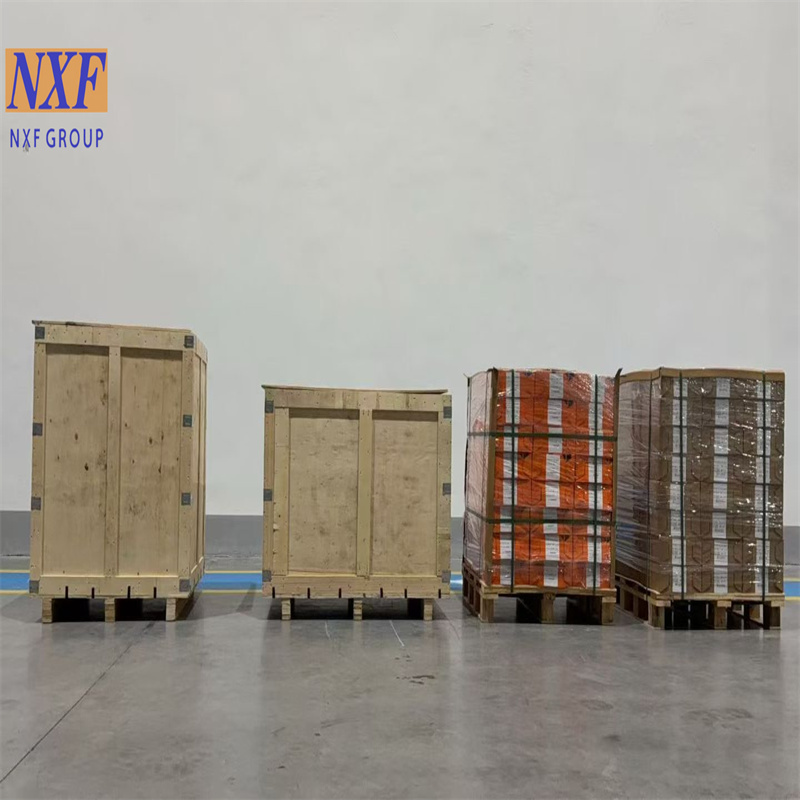
7. Marking, Packaging, and DeliveryConforming finished flanges are marked with specifications, dimensions, standards, and furnace number.Each product is packaged with rust-proof materials. Flanges are neatly packed in wooden crates with securing protective devices to prevent damage from impacts during long-distance transportation. A complete production process record is delivered with the goods.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
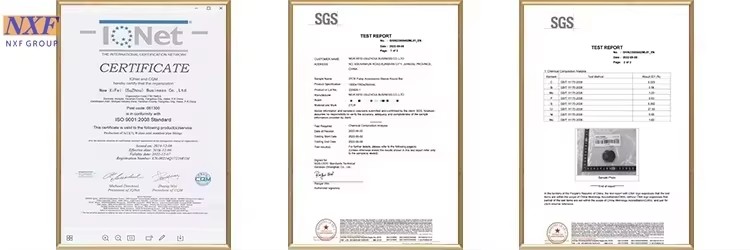
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.


Established in 1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolute customer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management and Craftsmanship."
Our advantage as follow:
1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service..



East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern
Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2.how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material)
We have our own factories, quality can be controlled seriously.
We Specialize in manufacturing about 21 years.
We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
LanguageSpoken:English,Chinese,Spanish,Russian


total 0 Sheet,Only 5 images can be uploaded, each less than 5m.