

Phone/Whatsapp:+8613917160311
Email: info@nxf-group.com
Email: Andrew@nxf-group.com
Email: Alice@nxf-group.com


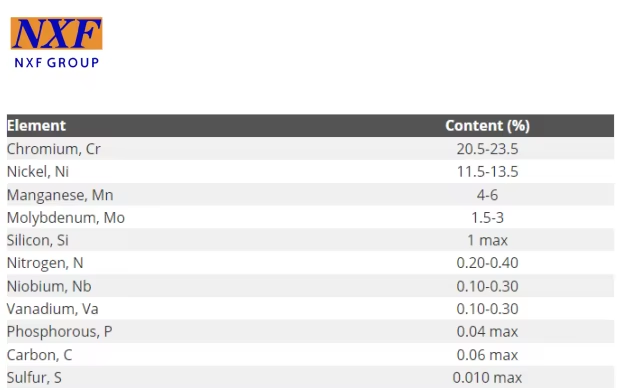
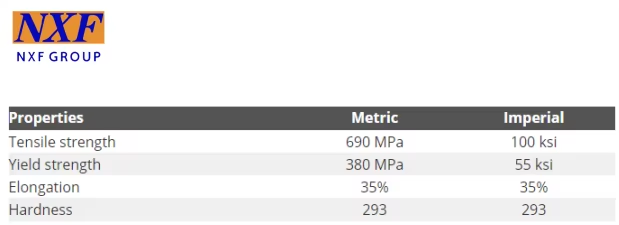
NXF UNS S20910 XM-19 Diameter DN15-1200 Pressure 150-2500lb Special Stainless Steel Forged Threaded Flanges
Threaded flanges are flanges that are connected to pipes via threads rather than welding. They have internal threads machined into their bore; installation simply involves screwing in a pipe with external threads to complete the connection. For materials with poor weldability or that cannot be welded (such as certain high-hardness alloy steels), threaded connections are an ideal alternative.
magneticpermeability of this alloy allows it to be used as a material for medical implants.
Machinability
Stainless steel grade UNS S20910 XM-19 has machinability characteristics that are similar to other austenitic stainless
steels;however it requires slower speeds, more power, and higher rigidity due to its high work hardening rate. It is recommended that coated carbide tooling be used.
Forming
Stainless steel grade UNS S20910 XM-19 can be formed using the same methods applied for other austenitic stainless steels. More power for forming and forging is needed for this alloy. Forging can be done at 1177-1204°C (2150-2200°F).
Welding
Welding of stainless steel grade UNS S20910 XM-19 can be performed using traditional joining processes. Recommended filler metal should be UNS S20910 XM-19 (AWS E/ER209).
Caution should be taken while using autogenous, high power density joining processes such as EB or laser welding, due to low FN potential and severe outgassing possibility.
Heat Treatment
Final annealing process performed for several of the applications, is done at 1065°C (1950°F), which is followed by water
quenching. In case this material is used in a strongly corrosive environment, annealing should be done at 1121°C (2050°F). This alloy cannot be hardened by heat treatment.





Product processing
1. Forging: Threaded flanges are typically forged using die forging or ring forging.Cutting and Heating: Heating the steel billet to a plastic state.Forging: Pressing the billet into a flange blank in a die, ensuring the metal flow lines follow the flange profile to improve pressure resistance.Punching: Punching away excess metal from the center to form a preliminary center through hole.
2. Heat Treatment:Normalizing/Annealing: Relieving forging stress. For stainless steel (e.g., 304/316L), solution treatment is required to ensure corrosion resistance; for carbon steel (e.g., A105), normalizing is often used to refine the grain size.
3. Precision Machining (CNC Machining) :
This is a crucial step determining the quality of the threaded flange, completed in multiple steps on a CNC lathe:Outer Diameter and Sealing Surface Machining: Machining the precise outer diameter and sealing water lines (e.g., the serrated pattern on the RF surface).Internal Hole Enlargement: Machining the internal hole to a precise pre-drilled size suitable for tapping.Threading:Core Step Using CNC cutting tools to cut NPT (American Standard Tapered Pipe Thread) or BSP/PT (European/British Standard Thread).Taper Control: NPT threads have a 1:16 taper; during machining, the taper must be precise to form a tight interference seal with the pipe.
4. DrillingUsing a CNC drilling machine or indexing table, drill bolt holes according to standards (such as ASME B16.5), ensuring the roundness of the hole positions and their coaxiality with the thread centerline.
5. Thread Inspection:
Threaded flanges require more stringent inspection than welded flanges:Gauge Inspection: Using a thread plug gauge for inspection. Typically, after manual screwing in, the flange end face should fall within the gauge's reference plane (+/- 1 thread).Go/No-Go Gauge Test: Ensures thread integrity and precision, preventing seizing or seal failure during assembly.
6. Surface Treatment and CleaningDeburring: Thoroughly removes metal residue from the thread grooves.Corrosion Protection: Carbon steel is phosphated, oiled, or galvanized to prevent threads from rusting during storage and becoming impossible to screw in.Key Points in Thread Machining Comparison:Sealing Oil/Tape: Although machining precision is high, users should still be reminded to use thread sealant or Teflon tape during installation.Wall Thickness Compensation: Machining threads weakens the pipe end strength; therefore, the flange neck thickness is usually slightly thicker than that of a flat-face flange of the same specifications during design and machining.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
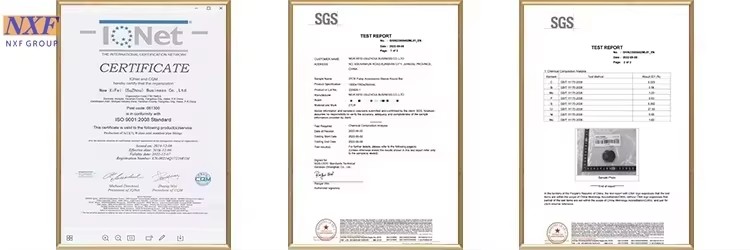
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service.



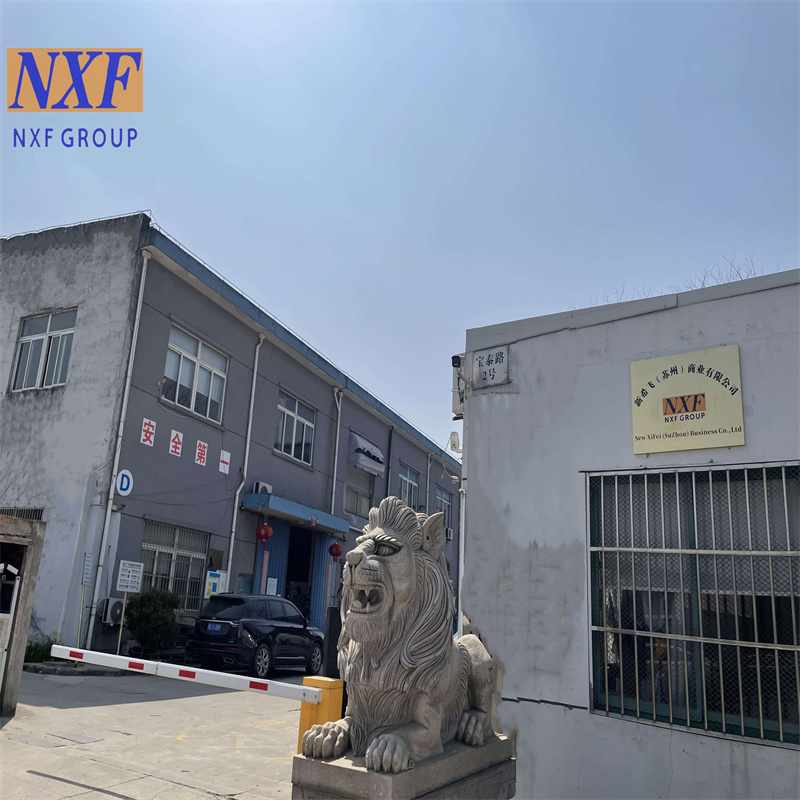
Established in 1980, XIFEI has been working diligently ever since to embrace the needs of our global customer base.We work to ensure absolute customer satisfaction. Our team has dedicated itself to perfecting our three core components, "Service, Management and Craftsmanship."
Our advantage as follow:
1.We have our own factory, and we can control the cost by producing by ourselves. We have a great advantage in price and can give you the lowest price.
2. We can strictly control the quality. We have production, quality inspection, warehousing and other departments to coordinate and control the quality.Such as PMI testing
3. Our biggest advantage is 3S service. Small quantity, short time, special materials.
4.We have excellent quality certificate system and trademark certificate
5.We have a comprehensive after-sales service guarantee, such as the transaction guarantee provided by Alibaba International Station, as well as remote technical guidance and services.
6.We have a well-established logistics support system that can save you both time and money, providing you with a one-stop service..



East(10.00%),Eastern Europe(10.00%),South America(10.00%),Domestic Market(5.00%),North America(5.00%),Northern
Europe(5.00%),Central America(5.00%),Africa(5.00%),Southeast Asia(5.00%). There are total about 101-200 people in our office.
2.how can we guarantee quality?
Always a pre-production sample before mass production;
Always final Inspection before shipment;
3.what can you buy from us?
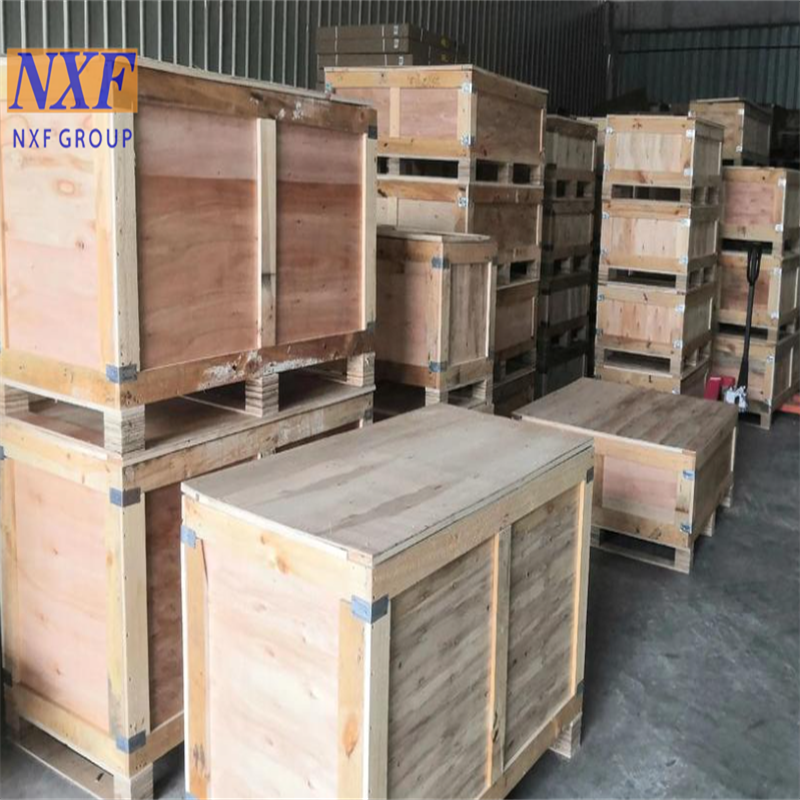
Pipe,Flange,Steel plate,Pipe fittings,Alloy products
4. why should you buy from us not from other suppliers?
Our advantage:3S Service (Small Quantity/Short Time/Special Material)
We have our own factories, quality can be controlled seriously.
We Specialize in manufacturing about 21 years.
We have professional testing department and testing equipment.
5. what services can we provide?
Accepted Delivery Terms: FOB,CFR,CIF,EXW,FCA,DDP,DDU;
Accepted Payment Currency:USD,EUR,CAD,HKD,CNY;
Accepted Payment Type: T/T,L/C,D/P D/A,Credit Card,PayPal;
LanguageSpoken:English,Chinese,Spanish,Russian


total 0 Sheet,Only 5 images can be uploaded, each less than 5m.